How does a downflow cartridge dust collector work? Dust-laden air enters the collector, larger particles are separated by airflow and gravity, fine dust is captured by filter cartridges, and pulse-jet compressed air cleans the filter surface. Learn how downflow airflow and cartridge filtration work together in industrial dust collection.
A downflow cartridge dust collector is designed to capture fine, dry particulate matter from industrial processes while directing the contaminated airflow downward through the filtration section. This airflow arrangement can help separated dust move toward the hopper and reduce unnecessary re-entrainment during filtration and pulse cleaning.
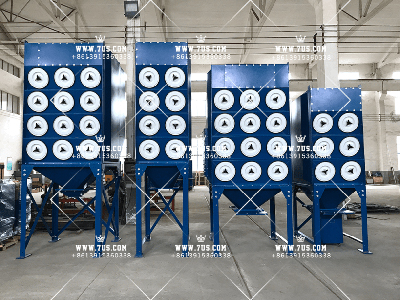
What Is a Downflow Cartridge Dust Collector?
A downflow cartridge dust collector uses pleated filter cartridges to capture particulate matter while the internal airflow is arranged to move generally downward through the dust collection section.
Cartridge filters provide a large filtration area within a relatively compact structure, making this type of dust collector suitable for many fine and dry industrial dust applications.
How Does a Downflow Cartridge Dust Collector Work?
The dust collection process can be divided into several stages: dust-laden air entry, preliminary particle separation, cartridge filtration, pulse-jet cleaning, and collected dust discharge.
1. Dust-Laden Air Enters the Collector
Contaminated air from the production process enters the dust collector through the inlet. The inlet and internal airflow arrangement help distribute the air through the collector before it reaches the filter cartridges.
Depending on particle characteristics and collector design, some larger and heavier particles can lose velocity and move downward toward the hopper before reaching the filter surface.
2. Fine Dust Is Captured by Filter Cartridges
Fine particulate matter remaining in the airflow reaches the pleated filter cartridges. Dust is captured on the outer surface of the filter media while filtered air passes through the cartridges.
Filter media can be selected according to dust characteristics, operating temperature, moisture, oil content, filtration requirements, and other process conditions.
3. Filtered Air Leaves the Dust Collector
After passing through the filter cartridges, the filtered airflow enters the clean-air section and leaves the collector through the outlet according to the equipment configuration.
The final filtration performance depends on the filter media, filter condition, equipment sealing, operating airflow, and overall system configuration.
4. Pulse-Jet Cleaning Removes Accumulated Dust
As dust accumulates on the cartridge surface, filtration resistance gradually increases. A pulse-jet cleaning system uses short bursts of compressed air to dislodge accumulated dust from the filters.
Pulse valves release compressed air according to the cleaning control sequence. Cleaning can be controlled by time, differential pressure, or other control logic depending on the equipment configuration.
5. Collected Dust Falls into the Hopper
Dust released from the filter surface moves downward into the hopper or dust collection section. The collected material can then be discharged into a bin, drum, rotary valve, screw conveyor, or another handling device depending on the equipment design.
What Is the Advantage of Downflow Airflow?
One advantage of a downflow arrangement is that the general direction of the contaminated airflow can assist the downward movement of separated dust toward the collection hopper.
During pulse cleaning, dust released from the cartridge surface can also move downward rather than being carried directly upward against the intended dust discharge direction.
Actual performance still depends on inlet design, internal airflow distribution, filter arrangement, particle characteristics, filtration velocity, and equipment configuration.
Downflow vs Conventional Cartridge Dust Collector: What Is the Difference?
Cartridge dust collectors can use different filter orientations and airflow arrangements. Downflow designs emphasize downward movement of dust-laden air through the filtration section, while other collectors may use crossflow or different internal airflow paths.
No single configuration is automatically suitable for every application. Equipment selection should consider dust characteristics, required airflow, installation space, filter arrangement, maintenance access, and operating conditions.
Where Are Downflow Cartridge Dust Collectors Used?
Downflow cartridge dust collectors can be used for suitable fine and dry dust generated by grinding, cutting, sanding, polishing, welding-related processes, powder handling, metalworking, woodworking, and other industrial manufacturing operations.
Applications involving significant moisture, oil mist, sticky dust, combustible materials, or other special conditions should be evaluated before selecting conventional dry cartridge filtration.
How Do You Choose a Downflow Cartridge Dust Collector?
Important information includes required airflow, dust type, particle characteristics, operating temperature, moisture or oil content, indoor or outdoor installation, voltage and frequency, and any special safety requirements.
Process photographs, capture hood information, duct conditions, and equipment drawings can also help clarify the required dust collector configuration.
Looking for a Downflow Cartridge Dust Collector Manufacturer?
Jiangsu Erhuan Environmental Technology Co., Ltd. manufactures industrial dust collection equipment and filtration products under the 7US brand for international markets. Our product range includes downflow and vertical cartridge dust collectors, baghouse dust collectors, wet dust collectors, industrial filter cartridges, and related filtration components.
We provide OEM and private-label manufacturing services for overseas distributors, engineering companies, system integrators, and equipment manufacturers.
If you are sourcing a downflow cartridge dust collector, provide the required airflow, dust characteristics, operating conditions, voltage and frequency, installation information, and required scope of supply for equipment evaluation.
View our industrial cartridge dust collectors for fine and dry dust applications.
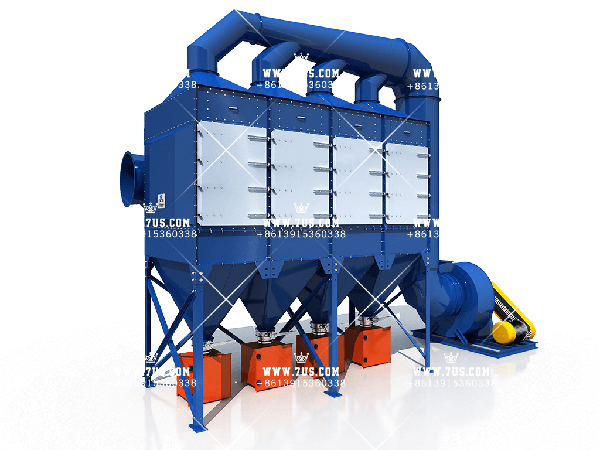
1. Vertical modular cartridge dust collector designed for high dust loading, fine dry dust and large-airflow industrial filtration applications. 2. Standardized DHC filtration modules can be combined to increase total airflow, allowing flexible system expansion according to project requirements. 3. Vertical cartridge arrangement with side-door access and eccentric cam fixing allows convenient filter inspection and replacement. 4. Single-stage cartridge filtration, two-stage cartridge + HEPA filtration, and three-stage cartridge + HEPA + activated carbon filtration configurations are available. 5. HEPA final filtration can be added for applications requiring very low particulate emissions, while activated carbon can be used as an additional polishing stage for suitable odor or VOC applications. 6. Standard single-module airflow ranges from 4,000 to 10,000 m³/h, and multiple DHC8 modules can be combined for systems up to 80,000 m³/h as shown on this page. 7. Equipment dimensions, filter media, color and OEM configuration can be customized according to project requirements.
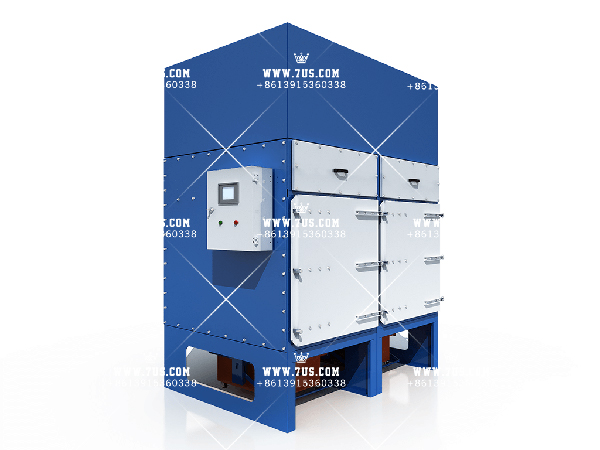
1. Vertical all-in-one cartridge dust collector designed for compact installation, convenient operation and efficient dry dust filtration. 2. Suitable for compatible dry dust and fume applications with dust-laden air temperatures below 120°C. 3. Vertical cartridge arrangement with side-door access allows convenient cartridge inspection and replacement. 4. Pleated cartridge filters provide a large filtration area within a compact equipment footprint, with automatic pulse-jet cleaning for routine filter cleaning. 5. Optional HEPA final filtration and activated carbon filtration can be added according to the required particulate and odor/VOC treatment needs. 6. DHC-YT series models are available with airflow capacities from 4,000 to 12,000 m³/h. 7. Equipment color, filter media, voltage, frequency and OEM configuration can be customized according to project requirements.
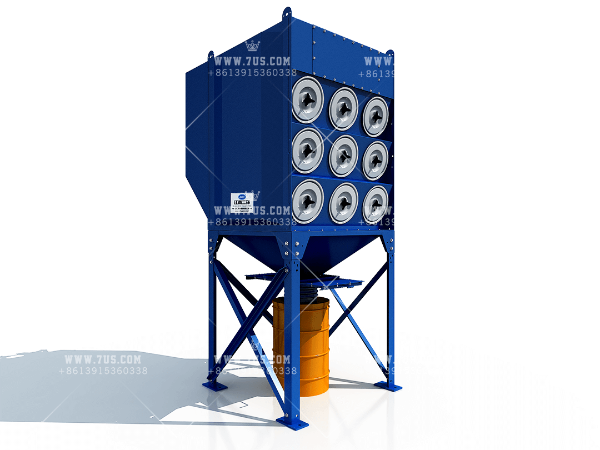
1. Downflow oblique modular cartridge dust collector designed for flexible capacity expansion through standardized modular units. 2. Compact modular construction helps reduce installation footprint and allows the equipment to be divided into transport-friendly sections for easier shipping and assembly. 3. Pleated cartridge filters provide a large filtration area within a compact equipment volume, with automatic pulse-jet cleaning for routine filter cleaning. 4. Standard EHDFT modules can be combined to increase total airflow according to project requirements, with configurations available up to 100,000 m³/h. 5. Optional two-stage filtration with cartridge filters and HEPA final filtration is available for applications requiring additional filtration performance. 6. Stainless steel construction, abrasion-resistant inlet arrangements, exhaust dampers and explosion protection components can be evaluated according to the application. 7. Suitable for compatible dry dust and fume applications without oil or water, subject to the confirmed dust characteristics and project safety requirements. 8. Equipment configuration, filter media, color a
No. 173, Wuwei Industrial Zone, Xushe Town, Yixing, Jiangsu, China© 1994-2026 7US.com. All rights reserved | Privacy PolicySite map
Phone