How can a flat bag dust collector handle high temperature chemical dust? This Yanchang Petroleum case study shows how industrial bag filtration equipment was applied to a chemical production process involving high temperature gas, high dust concentration, and calcium carbonate recovery.
High temperature chemical processes can create challenging dust collection conditions involving elevated gas temperatures, high dust concentrations, and process-specific particulate matter. In this project, Jiangsu Erhuan Environmental Technology Co., Ltd. supplied a flat bag dust collector for a Yanchang Petroleum application in Yulin, Shaanxi.

Industrial Dust Collection Case Study: Yanchang Petroleum
The application involved a chemical production process in which process materials were handled under high temperature conditions. According to the original project record, the operating gas temperature associated with the dust collection process was approximately 240°C.
The flat bag dust collector was used to collect particulate matter generated during the process after the required chemical reaction and process conditions were established.
Why Use a Flat Bag Dust Collector for Chemical Dust?
Industrial chemical processes can generate high concentrations of particulate matter and may involve elevated temperatures. Bag filtration provides a large filtration area and allows different filter media to be selected according to temperature, dust characteristics, chemical conditions, and filtration requirements.
A flat bag dust collector uses compact filter elements that can provide substantial filtration area within the collector housing, making this type of equipment suitable for selected industrial applications where installation space and filtration requirements must be considered together.
How Does High Temperature Affect Dust Collector Selection?
Temperature is one of the most important parameters when selecting a baghouse dust collector. Standard filter media cannot be used safely under every high temperature condition.
Filter media such as aramid, PPS, or other specialized materials may be selected according to the actual continuous operating temperature, peak temperature, chemical composition, moisture, and other process conditions.
The complete equipment configuration should therefore be based on the actual inlet conditions rather than simply selecting a dust collector by airflow or physical size.
What Are the Challenges of High Concentration Dust?
High dust concentration increases the dust loading on filtration equipment. Sufficient filtration area, appropriate air-to-cloth ratio, reliable filter cleaning, hopper design, and dust discharge capacity are important considerations for stable operation.
Pulse-jet cleaning can be used to remove accumulated dust from filter elements and help maintain stable pressure drop during continuous industrial operation.
Can a Dust Collector Support Material Recovery?
In some chemical and mineral processing applications, collected particulate matter may have recycling or recovery value. A properly selected industrial dust collection system can therefore serve both particulate filtration and material recovery objectives, depending on the production process.
Dust characteristics and downstream handling requirements should be evaluated when determining the appropriate collection and discharge method.
What Information Is Needed for a Chemical Dust Collector?
Before selecting dust collection equipment for a chemical process, important information includes required airflow, dust type, dust concentration, inlet temperature, moisture, chemical characteristics, filter media requirements, installation conditions, voltage and frequency, and applicable safety requirements.
Process drawings and equipment layout information can also help clarify the required dust collector configuration.
Looking for a High Temperature Bag Dust Collector Manufacturer?
Jiangsu Erhuan Environmental Technology Co., Ltd. manufactures industrial dust collection equipment and filtration products under the 7US brand for international markets. Our product range includes flat bag dust collectors, conventional baghouse dust collectors, cartridge dust collectors, wet dust collectors, industrial filter bags, filter cartridges, and related filtration components.
We provide OEM and private-label manufacturing services for overseas distributors, engineering companies, system integrators, and equipment manufacturers.
If you are sourcing a dust collector for high temperature chemical or industrial dust, provide the required airflow, dust characteristics, inlet temperature, process conditions, electrical requirements, and required scope of supply for equipment evaluation.
View our flat bag dust collectors for industrial dust collection applications.
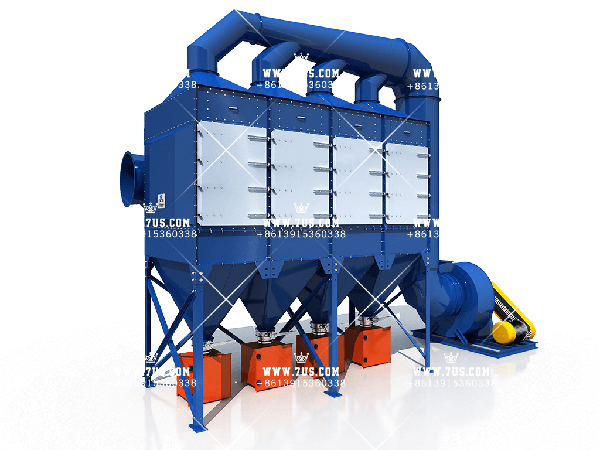
1. Vertical modular cartridge dust collector designed for high dust loading, fine dry dust and large-airflow industrial filtration applications. 2. Standardized DHC filtration modules can be combined to increase total airflow, allowing flexible system expansion according to project requirements. 3. Vertical cartridge arrangement with side-door access and eccentric cam fixing allows convenient filter inspection and replacement. 4. Single-stage cartridge filtration, two-stage cartridge + HEPA filtration, and three-stage cartridge + HEPA + activated carbon filtration configurations are available. 5. HEPA final filtration can be added for applications requiring very low particulate emissions, while activated carbon can be used as an additional polishing stage for suitable odor or VOC applications. 6. Standard single-module airflow ranges from 4,000 to 10,000 m³/h, and multiple DHC8 modules can be combined for systems up to 80,000 m³/h as shown on this page. 7. Equipment dimensions, filter media, color and OEM configuration can be customized according to project requirements.
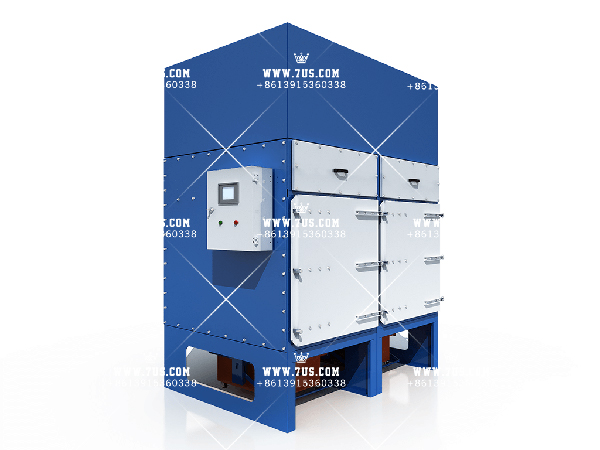
1. Vertical all-in-one cartridge dust collector designed for compact installation, convenient operation and efficient dry dust filtration. 2. Suitable for compatible dry dust and fume applications with dust-laden air temperatures below 120°C. 3. Vertical cartridge arrangement with side-door access allows convenient cartridge inspection and replacement. 4. Pleated cartridge filters provide a large filtration area within a compact equipment footprint, with automatic pulse-jet cleaning for routine filter cleaning. 5. Optional HEPA final filtration and activated carbon filtration can be added according to the required particulate and odor/VOC treatment needs. 6. DHC-YT series models are available with airflow capacities from 4,000 to 12,000 m³/h. 7. Equipment color, filter media, voltage, frequency and OEM configuration can be customized according to project requirements.
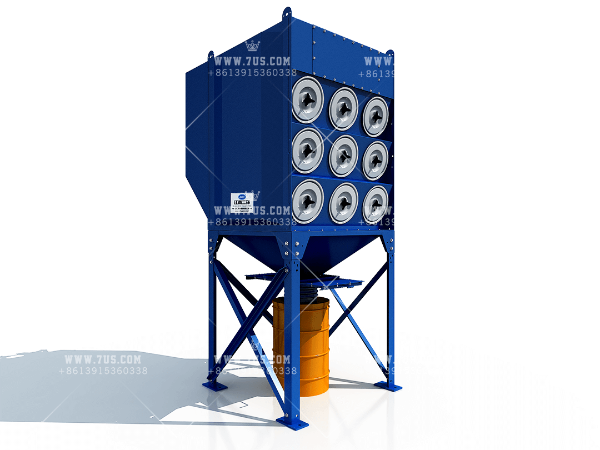
1. Downflow oblique modular cartridge dust collector designed for flexible capacity expansion through standardized modular units. 2. Compact modular construction helps reduce installation footprint and allows the equipment to be divided into transport-friendly sections for easier shipping and assembly. 3. Pleated cartridge filters provide a large filtration area within a compact equipment volume, with automatic pulse-jet cleaning for routine filter cleaning. 4. Standard EHDFT modules can be combined to increase total airflow according to project requirements, with configurations available up to 100,000 m³/h. 5. Optional two-stage filtration with cartridge filters and HEPA final filtration is available for applications requiring additional filtration performance. 6. Stainless steel construction, abrasion-resistant inlet arrangements, exhaust dampers and explosion protection components can be evaluated according to the application. 7. Suitable for compatible dry dust and fume applications without oil or water, subject to the confirmed dust characteristics and project safety requirements. 8. Equipment configuration, filter media, color a
No. 173, Wuwei Industrial Zone, Xushe Town, Yixing, Jiangsu, China© 1994-2026 7US.com. All rights reserved | Privacy PolicySite map
Phone