How is a high temperature bag filter used in an RTO project? This case study shows how industrial baghouse dust collection equipment was applied to capture valuable metal-containing dust downstream of a chemical waste liquid RTO process after gas cooling.
High temperature industrial processes can require specialized dust collection equipment, especially when the exhaust gas contains valuable or difficult-to-handle particulate matter. In this project, a high temperature bag filter was supplied for a chemical waste liquid RTO application.
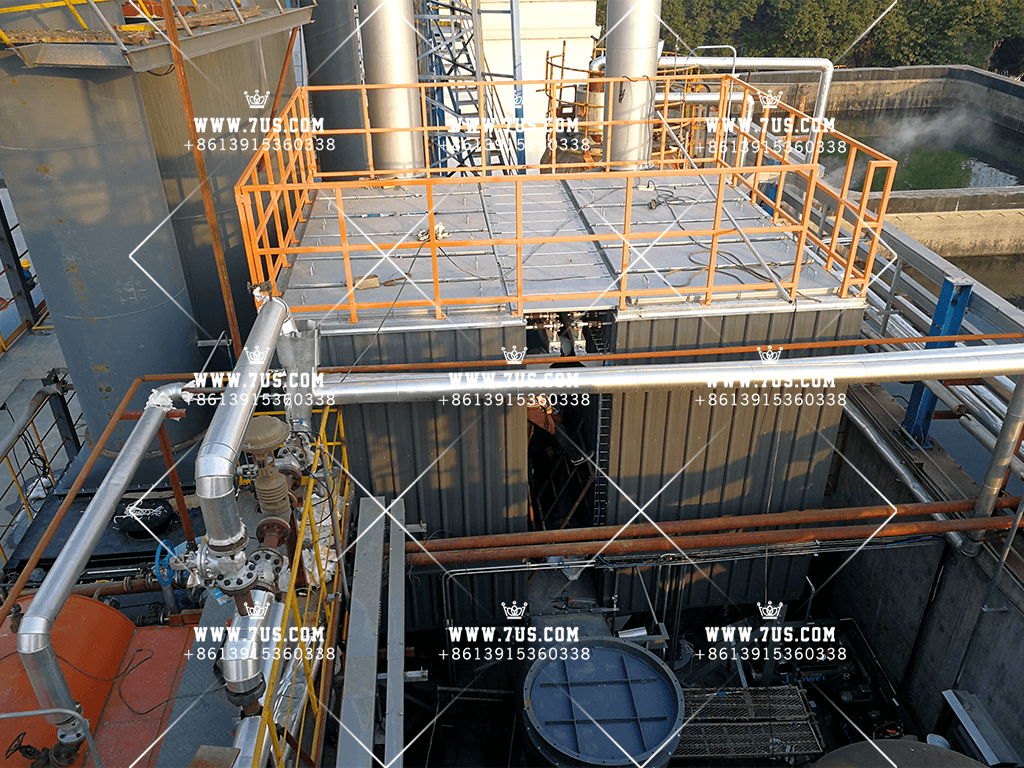
Project Application: RTO Dust Collection
The project involved Nanjing Changjiang Jiangyu Petrochemical Co., Ltd. and a chemical waste liquid RTO combustion process. During operation, the RTO process generated dust containing valuable metal compounds, including cobalt oxide.
The exhaust gas temperature after combustion could reach approximately 700°C. Before entering the baghouse dust collector, the gas was cooled by upstream process equipment to approximately 230°C.
The high temperature bag filter was then used to capture particulate matter from the cooled gas stream.
Why Was a High Temperature Bag Filter Required?
Standard dust collection equipment and filter media are not suitable for every high temperature application. Gas temperature, dust characteristics, chemical conditions, filtration requirements, and filter media temperature resistance must all be considered before selecting an industrial baghouse dust collector.
In this RTO dust collection application, the upstream cooling process reduced the exhaust temperature before filtration, while the bag filter provided the required particulate collection stage.
Recovering Valuable Dust from the RTO Process
Dust collection in this project was not only intended for particulate control. The collected material contained valuable metal compounds, giving the dust recovery process additional resource value.
This illustrates an important benefit of industrial dust collection systems: depending on the production process and collected material, a baghouse dust collector can support both particulate filtration and material recovery.
What Should Be Considered for High Temperature Baghouse Dust Collection?
High temperature baghouse applications require careful evaluation of the actual operating conditions. Important parameters include inlet gas temperature, dust characteristics, required airflow, dust concentration, moisture, chemical composition, filter media, and system pressure conditions.
Filter media selection is particularly important. Different high temperature applications may require aramid, PPS, or other specialized filter materials according to the actual temperature and chemical environment.
Can a Bag Filter Handle 700°C Gas Directly?
No. The approximately 700°C temperature in this project refers to the high-temperature gas generated by the upstream RTO combustion process. The gas was cooled to approximately 230°C before entering the bag filter.
This distinction is important when evaluating a high temperature dust collection system. The allowable inlet temperature of the dust collector depends on the filter media, equipment construction, and actual operating conditions.
High Temperature Bag Filter Manufacturer for Industrial Projects
Jiangsu Erhuan Environmental Technology Co., Ltd. manufactures industrial dust collection equipment and filtration products under the 7US brand for international markets. Our product range includes baghouse dust collectors, cartridge dust collectors, wet dust collectors, industrial filter cartridges, filter bags, and related filtration components.
We provide OEM and private-label manufacturing services for overseas distributors, engineering companies, system integrators, and equipment manufacturers.
For high temperature baghouse projects, customers can provide the required airflow, inlet temperature, dust characteristics, moisture or chemical conditions, filter media requirements, electrical specifications, and equipment drawings for equipment evaluation.
View our industrial baghouse dust collection equipment for different process applications.
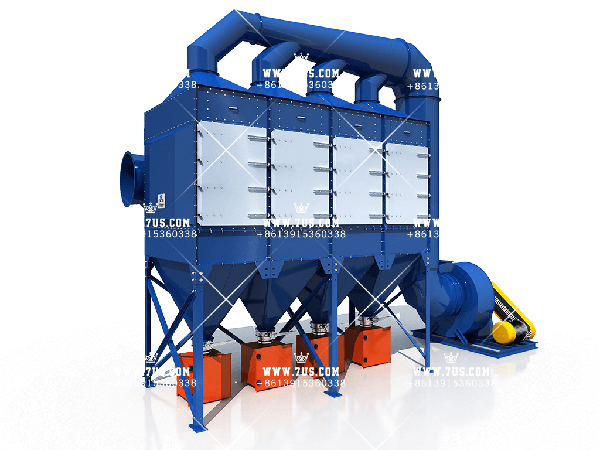
1. Vertical modular cartridge dust collector designed for high dust loading, fine dry dust and large-airflow industrial filtration applications. 2. Standardized DHC filtration modules can be combined to increase total airflow, allowing flexible system expansion according to project requirements. 3. Vertical cartridge arrangement with side-door access and eccentric cam fixing allows convenient filter inspection and replacement. 4. Single-stage cartridge filtration, two-stage cartridge + HEPA filtration, and three-stage cartridge + HEPA + activated carbon filtration configurations are available. 5. HEPA final filtration can be added for applications requiring very low particulate emissions, while activated carbon can be used as an additional polishing stage for suitable odor or VOC applications. 6. Standard single-module airflow ranges from 4,000 to 10,000 m³/h, and multiple DHC8 modules can be combined for systems up to 80,000 m³/h as shown on this page. 7. Equipment dimensions, filter media, color and OEM configuration can be customized according to project requirements.
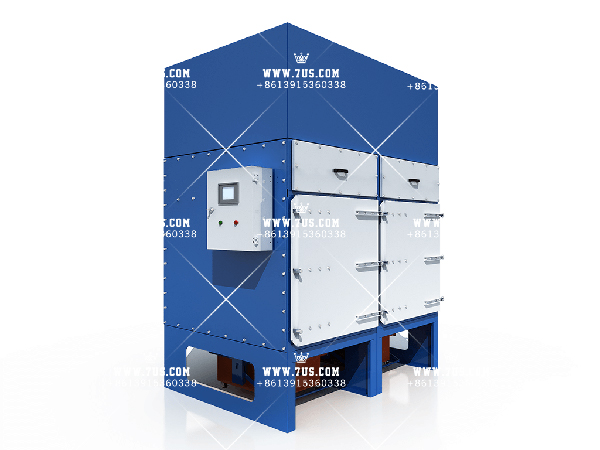
1. Vertical all-in-one cartridge dust collector designed for compact installation, convenient operation and efficient dry dust filtration. 2. Suitable for compatible dry dust and fume applications with dust-laden air temperatures below 120°C. 3. Vertical cartridge arrangement with side-door access allows convenient cartridge inspection and replacement. 4. Pleated cartridge filters provide a large filtration area within a compact equipment footprint, with automatic pulse-jet cleaning for routine filter cleaning. 5. Optional HEPA final filtration and activated carbon filtration can be added according to the required particulate and odor/VOC treatment needs. 6. DHC-YT series models are available with airflow capacities from 4,000 to 12,000 m³/h. 7. Equipment color, filter media, voltage, frequency and OEM configuration can be customized according to project requirements.
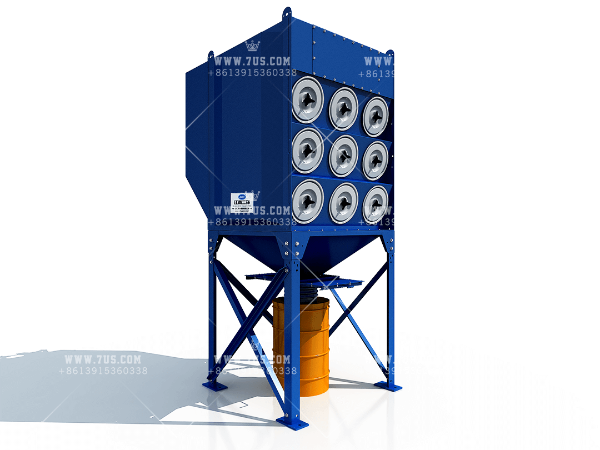
1. Downflow oblique modular cartridge dust collector designed for flexible capacity expansion through standardized modular units. 2. Compact modular construction helps reduce installation footprint and allows the equipment to be divided into transport-friendly sections for easier shipping and assembly. 3. Pleated cartridge filters provide a large filtration area within a compact equipment volume, with automatic pulse-jet cleaning for routine filter cleaning. 4. Standard EHDFT modules can be combined to increase total airflow according to project requirements, with configurations available up to 100,000 m³/h. 5. Optional two-stage filtration with cartridge filters and HEPA final filtration is available for applications requiring additional filtration performance. 6. Stainless steel construction, abrasion-resistant inlet arrangements, exhaust dampers and explosion protection components can be evaluated according to the application. 7. Suitable for compatible dry dust and fume applications without oil or water, subject to the confirmed dust characteristics and project safety requirements. 8. Equipment configuration, filter media, color a
No. 173, Wuwei Industrial Zone, Xushe Town, Yixing, Jiangsu, China© 1994-2026 7US.com. All rights reserved | Privacy PolicySite map
Phone