7US 7US Industrial dust collector since 1994

Downflow Cartridge Dust Collectors

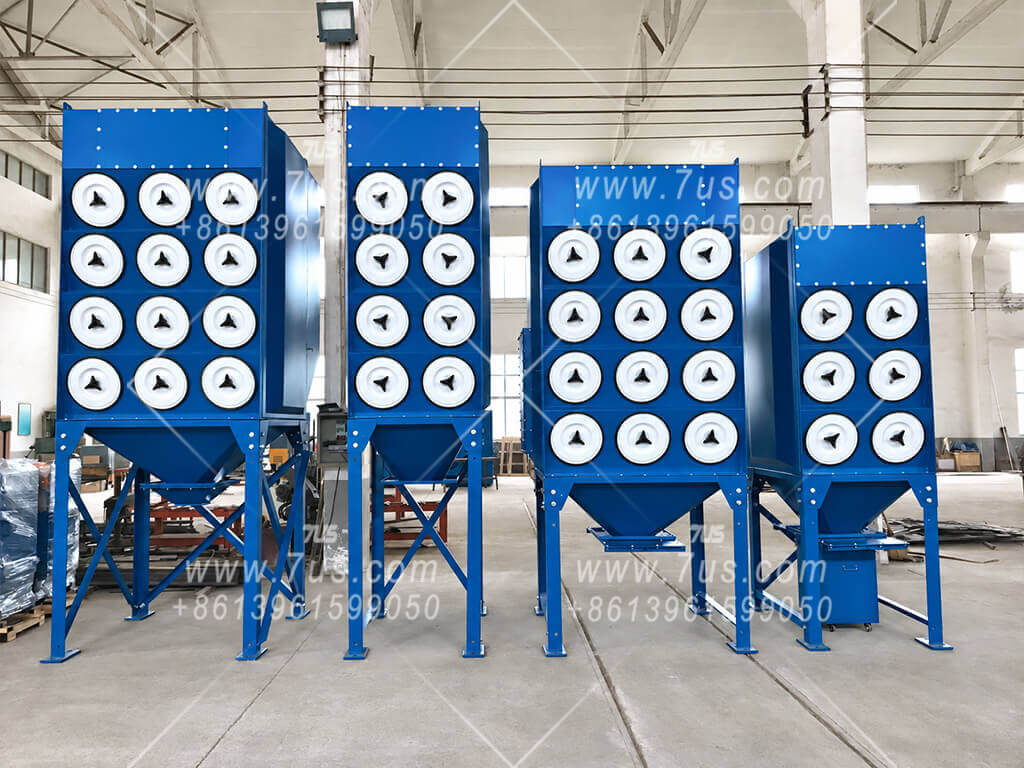
Modular downflow dust collectors available with inclined or horizontal cartridge arrangements, pulse-jet cleaning and flexible module combinations for industrial airflow requirements.

  • Inclined or horizontal cartridge arrangement
  • Automatic pulse-jet cleaning
  • Single or multi-module configurations
  • Fan, discharge & HEPA options
Downflow cartridge dust collector series
Open/Open CartridgeØ352 × 660 mm typical size
Pulse-Jet CleaningAutomatic filter cleaning
Modular ConstructionEasy capacity expansion
OEM AvailableRAL color / private label options
01Configurations
Contents ↑

Available Configurations

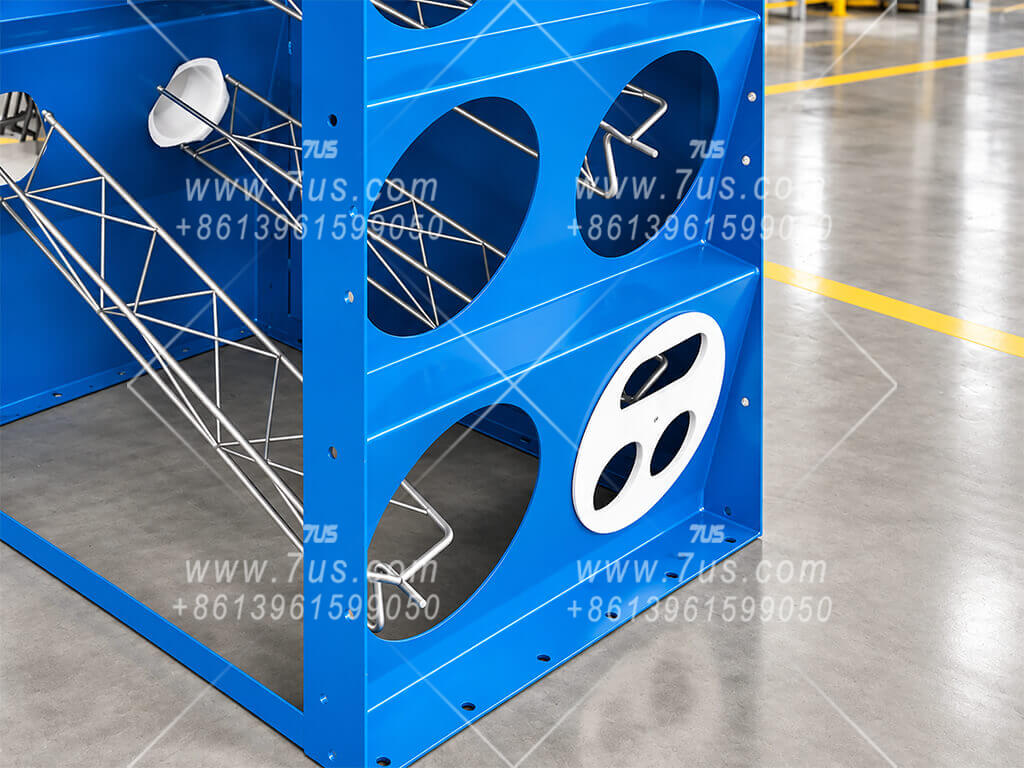
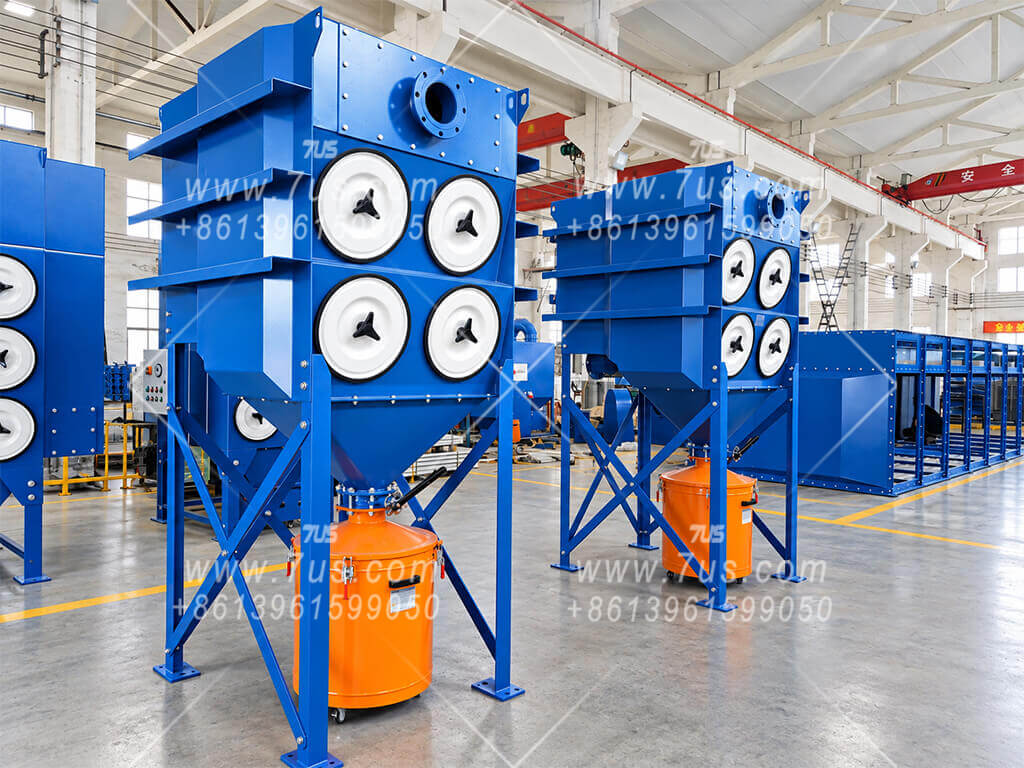
7US downflow cartridge dust collectors are available with horizontal or inclined cartridge arrangements. The inclined cartridge configuration is designed to reduce shelf-like dust accumulation on the filter surface and support more effective dust shedding during pulse-jet cleaning.

01 · CONVENTIONAL DESIGN

Horizontal Cartridge Arrangement

A simple and economical side-access layout with horizontally mounted cartridges. Manufacturing is straightforward, although dust is more likely to remain on the upper cartridge surface.

02 · IMPROVED DUST-SHEDDING DESIGN

Inclined Cartridge Arrangement

The inclined layout reduces the horizontal surface where dust can accumulate, helping released dust move away from the cartridges more effectively during pulse cleaning.

03

Modular Units

Standard collector modules can operate individually or be combined to increase filtration area and airflow capacity for larger systems.

04

Integrated Units

Compact all-in-one units combine the dust collector, fan and control components into a coordinated package for simpler installation and smaller airflow duties.

02How It Works
Contents ↑
HOW IT WORKS

Downflow Filtration & Pulse Cleaning

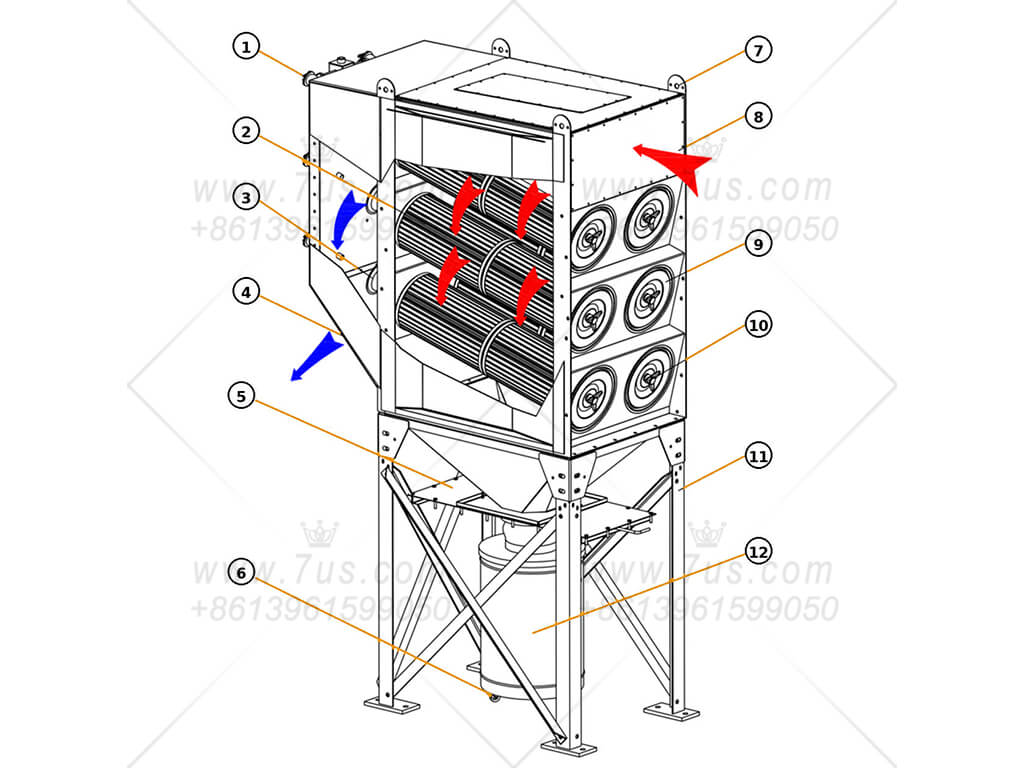
Horizontal and inclined downflow cartridge dust collector configurations use the same basic filtration and pulse-jet cleaning principle. The main difference is cartridge orientation: once the dust cake is released, the inclined arrangement provides less shelf-like surface for dust to remain on the cartridges.

Earlier configuration

Horizontal Cartridge Arrangement
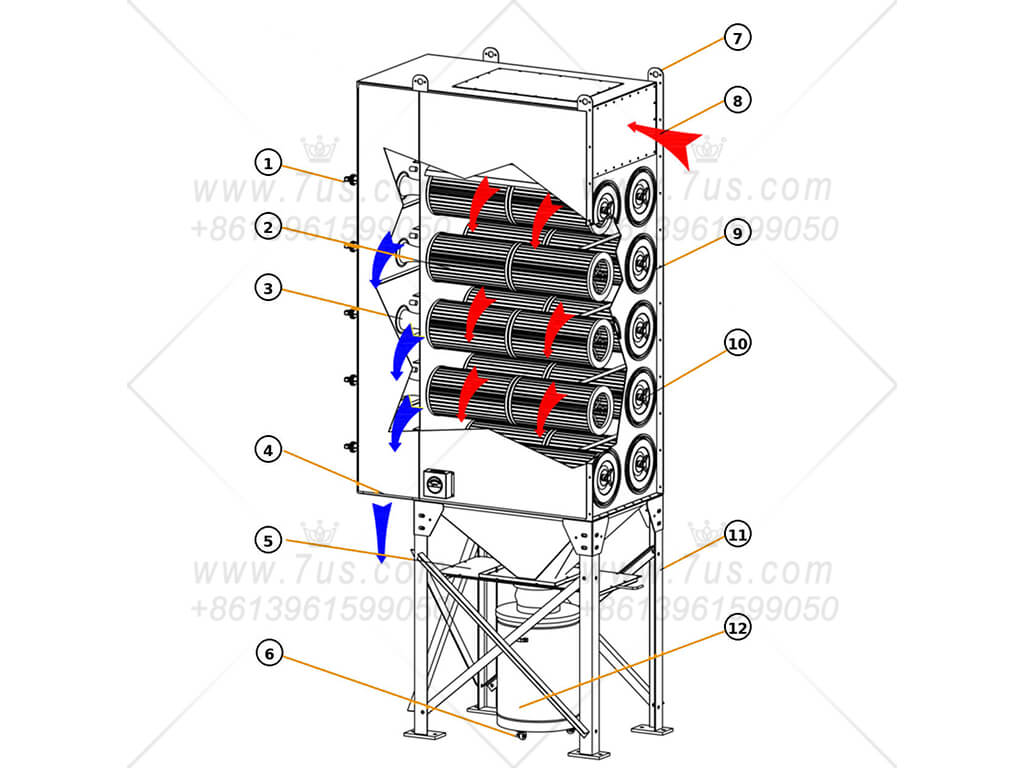
Horizontal cartridge dust collector arrangement with numbered component callouts

Horizontal: the level upper surface provides more area where released dust can settle again after pulse cleaning.
Current focus

Inclined Cartridge Arrangement

Inclined cartridge dust collector arrangement with numbered component callouts

Inclined: the angled cartridge surface helps released dust move away more naturally, allowing gravity and downflow to carry it toward the dust collection section.

Component Legend — Both Models
1Pulse Valve
2Filter Cartridge
3Venturi
4Air Outlet
5Slide Gate
6Caster Wheel
7Lifting Lug
8Dust-Laden Air Inlet
9Filter Cover
10Triangle Handle
11Support Leg
12Dust Collection Drum
01 / Normal Filtration

Normal Filtration

Dust-laden air enters the collector and flows through the cartridge section. Dust is retained on the outer cartridge surface, while cleaned air passes through the filter media and exits through the clean-air side of the collector.

02 / Pulse Cleaning

Pulse Cleaning

A short pulse of compressed air is injected from the clean-air side into the cartridges. This reverse pulse releases the dust cake from the outer filter surface so it can fall toward the dust collection drum.

03 / Why the Inclined Angle Matters

Why the Inclined Angle Matters

Once the dust cake is released, an inclined cartridge gives the particles less horizontal area to rest on. Gravity and downward airflow can therefore help the released dust leave the filter zone more easily.

03Cartridge Sealing
Contents ↑
SEALING DESIGN & MANUFACTURING PRECISION

Cartridge Sealing Reflects Manufacturing Accuracy

Both arrangements use two cartridges installed in series on the same support frame. The visible difference is how sealing pressure is achieved — and that difference is closely related to dimensional control, cartridge alignment, cover-plate fit and consistent gasket compression.
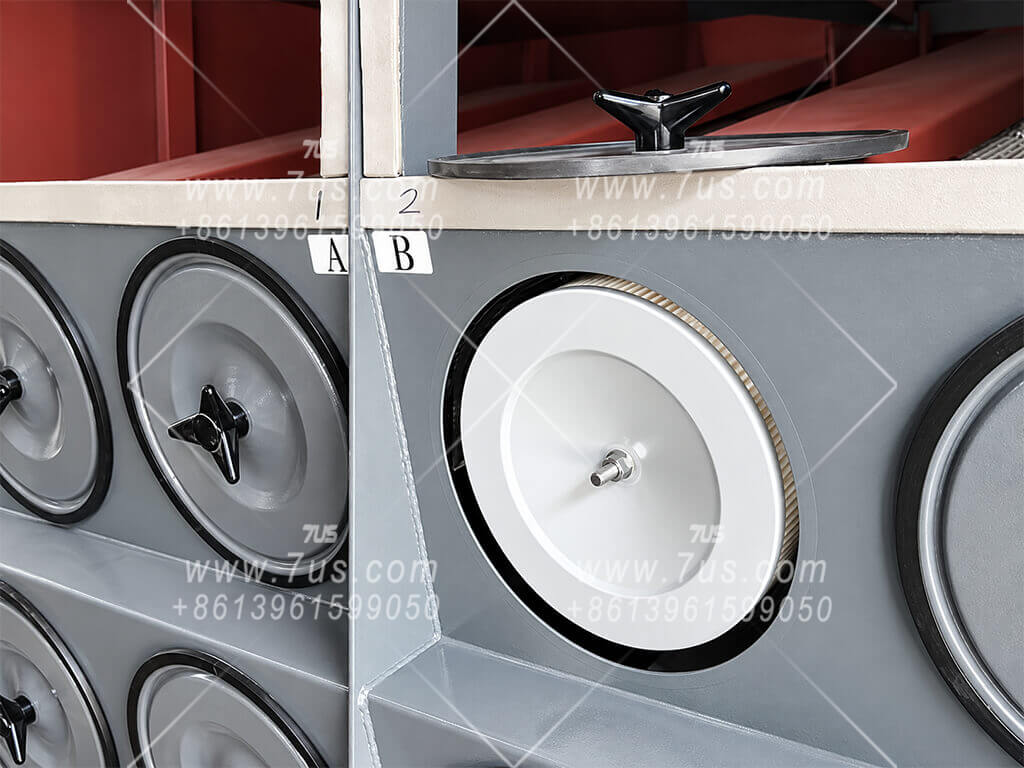
REFERENCE ARRANGEMENT

Additional Internal Center Nut Required

Open-open plus open-closed cartridge pair with center-nut sealing
01Cover Plate + Gasket + Internal Center Nut

Two cartridges are installed in series on the same support frame. The cover plate, gasket, center rod and external three-lobe handle are all present, while an additional internal center nut is also used to provide cartridge clamping. During cartridge replacement, this internal nut must be removed and re-tightened before the cover is secured again.
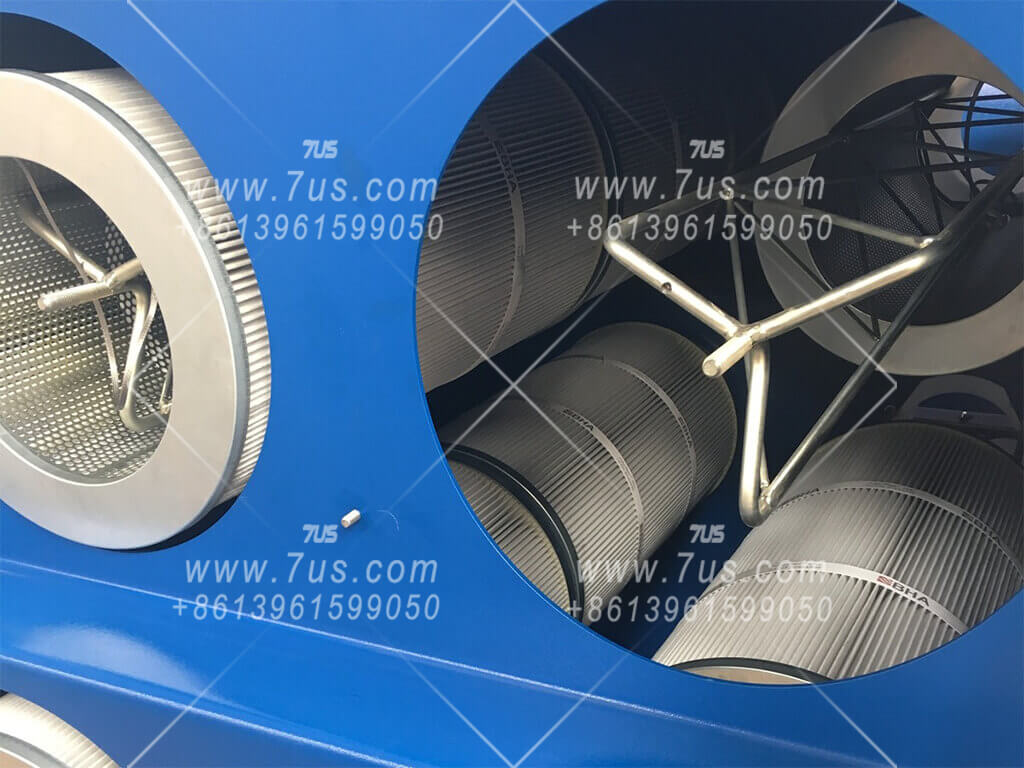
7US STANDARD DESIGN

Precision Cover-Plate & Gasket Sealing

7US open-open cartridge pair sealed by cover plate and gasket without center nut
02No Internal Center Nut Required

Two open/open cartridges are installed in series on the same support frame. Precise cartridge positioning, support-frame alignment and controlled gasket compression allow the cover plate to provide the required sealing pressure without an internal center nut. The center rod remains in place for the external three-lobe handle that locks the cover plate, while routine cartridge replacement avoids the extra internal nut-removal and re-tightening operation.

Reliable sealing starts with manufacturing accuracy — not with adding more fasteners.
Both designs use two cartridges in series, but the 7US arrangement achieves sealing through precise cartridge positioning, support-frame alignment, cover-plate fit and controlled gasket compression, so no additional internal center nut is required. For experienced dust-collection professionals, the cartridge sealing structure is one visible indicator of manufacturing precision and assembly quality.
04Modular Construction
Contents ↑
MODULAR CONSTRUCTION

What Makes a Collector Truly Modular

A segmented front appearance does not always mean a true modular cartridge dust collector. The real difference is at the connection interface: whether each section is fabricated as an independent structural module and then mechanically joined to the next module.

WHY MODULAR?

Control Welding Distortion Before Controlling the Whole Collector

ONE LARGE FULLY WELDED CABINET

Cumulative distortion becomes harder to control as the collector gets larger.

A very large continuous enclosure requires more welding across a longer structure. As weld length and heat input increase, shrinkage and dimensional drift can accumulate across the cabinet, making final alignment more difficult to control.

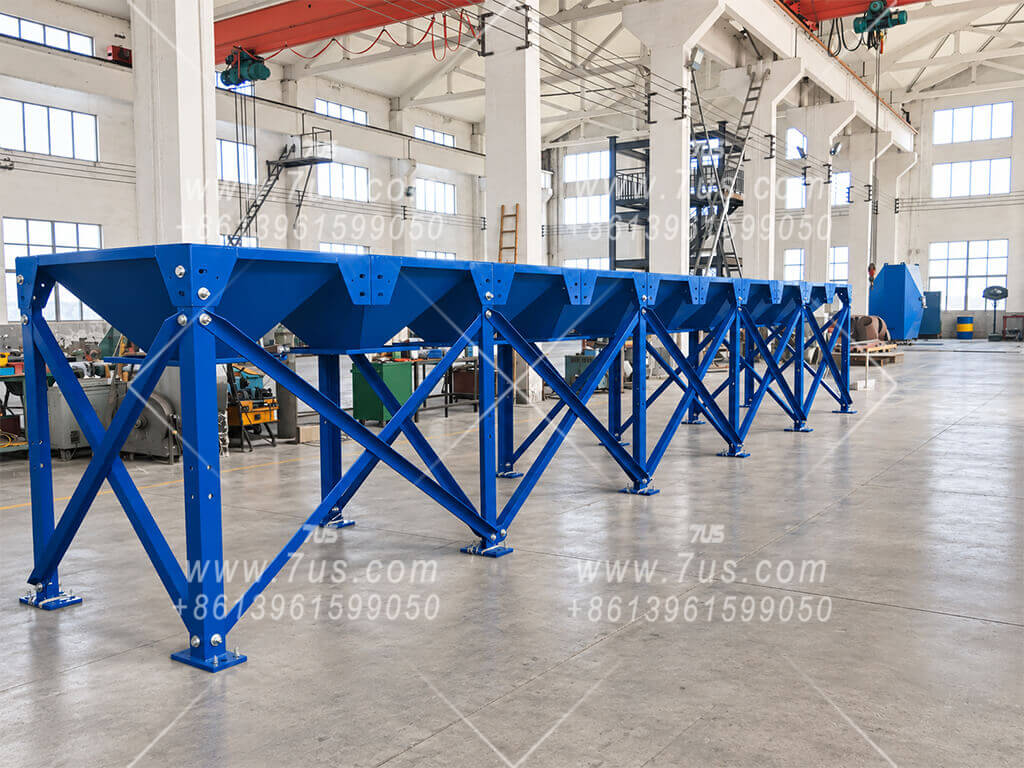
More weld length→More heat input→Harder cumulative control
→
7US INDEPENDENT MODULES

Each module is fully welded and dimensionally controlled before final assembly.

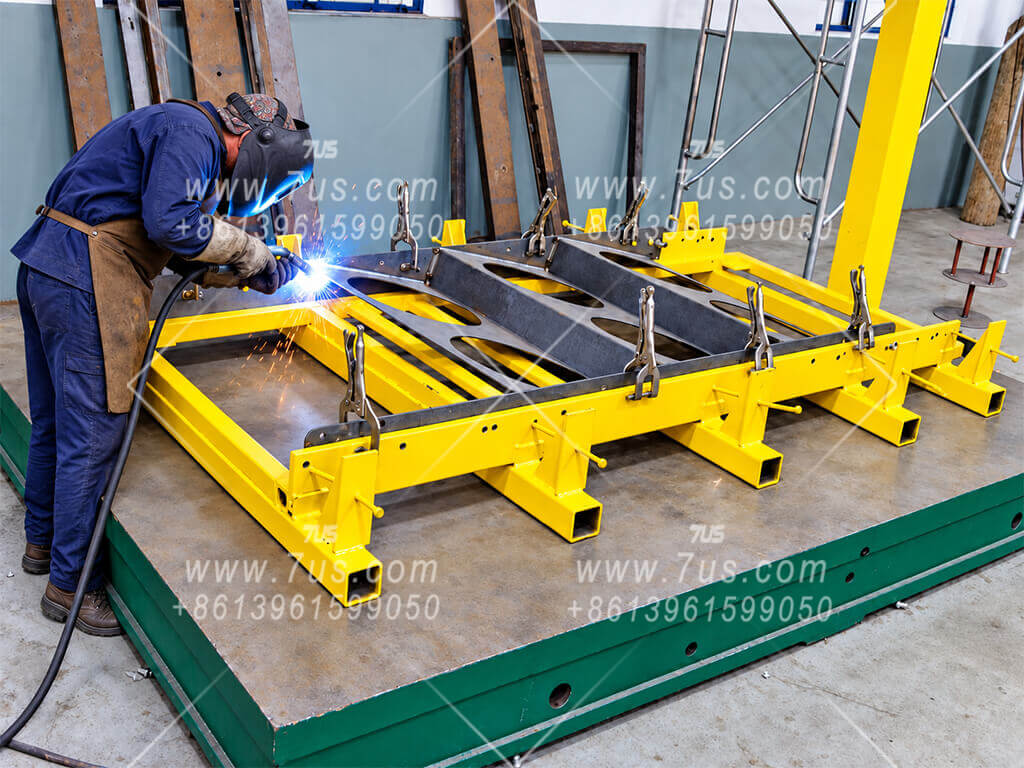
7US divides a large collector into repeatable structural modules. Each module is welded in dedicated fixtures, checked as an individual unit, and only then sealed and bolted to adjoining modules. This keeps welding distortion localized and helps reduce cumulative dimensional error across a large collector.
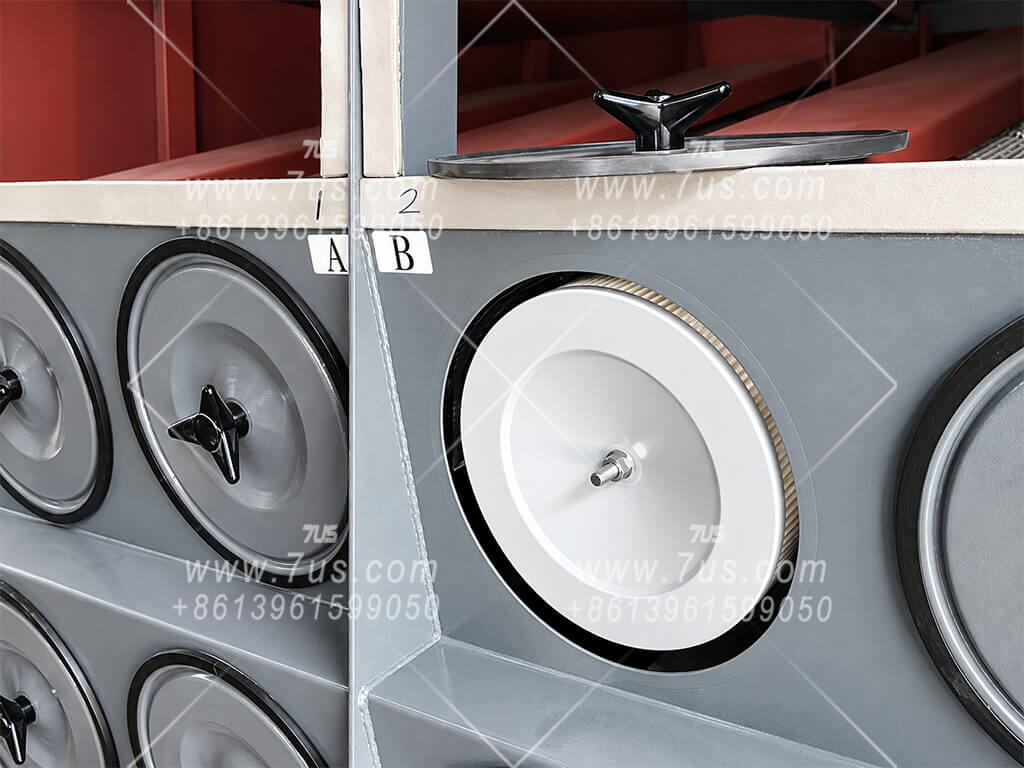
Fixture welding→Module inspection→Controlled final fit-up
Modular construction is therefore a manufacturing-control strategy, not only a transport or installation feature. Smaller repeatable welding units are easier to fixture, inspect and keep dimensionally consistent before they are combined into a large collector.
REFERENCE CONSTRUCTION

Integrated Cabinet with Modular Appearance

Visual division does not necessarily create an independent structural module.
Integrated cabinet with a visible divider or reinforcement strip
Visual divider / reinforcement on a continuous cabinet
Continuous cabinet with repeated cartridge rows and no true module joint
Repeated cartridge layout without a true structural module joint

These layouts can create a modular-looking front face while the main enclosure remains largely continuous. A divider, reinforcement strip or repeated cartridge pattern does not by itself prove that two independently fabricated modules have been structurally joined.
Continuous or largely integrated cabinet body
Visual divider or reinforcement may create a segmented appearance
No clear independent module-to-module bolted interface
7US STANDARD CONSTRUCTION

True Bolted Modular Construction

Independent structural modules with real mating surfaces and mechanical fastening.
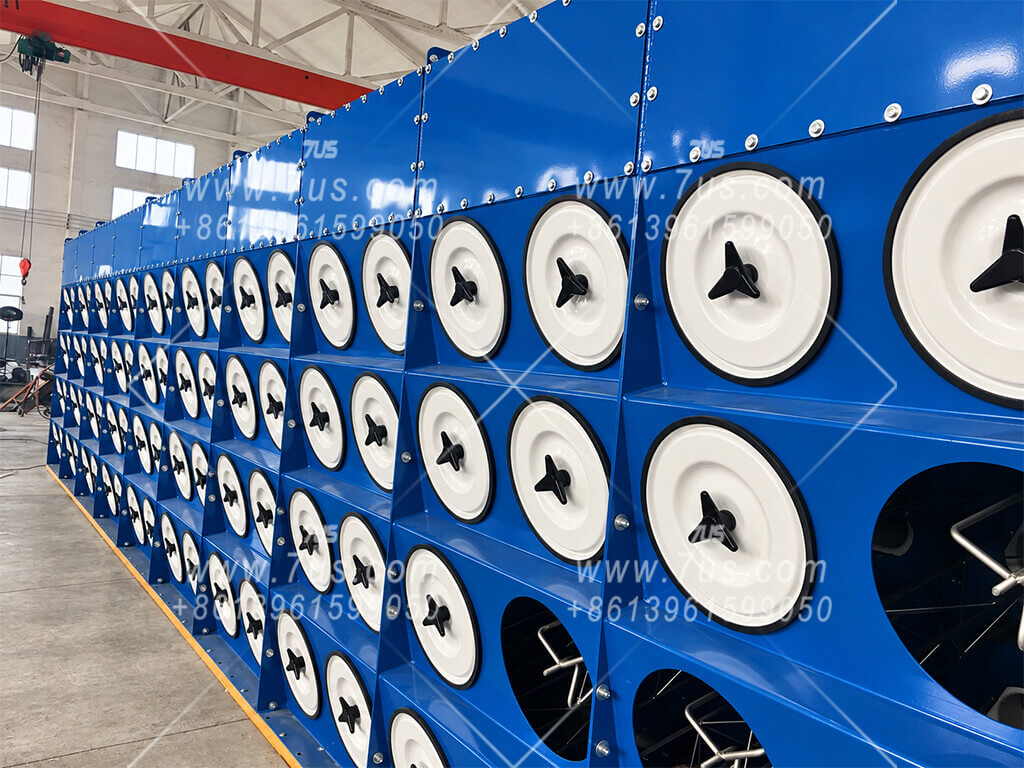
7US independent dust collector modules assembled side by side
Real module boundaries and bolted joints on a 7US collector
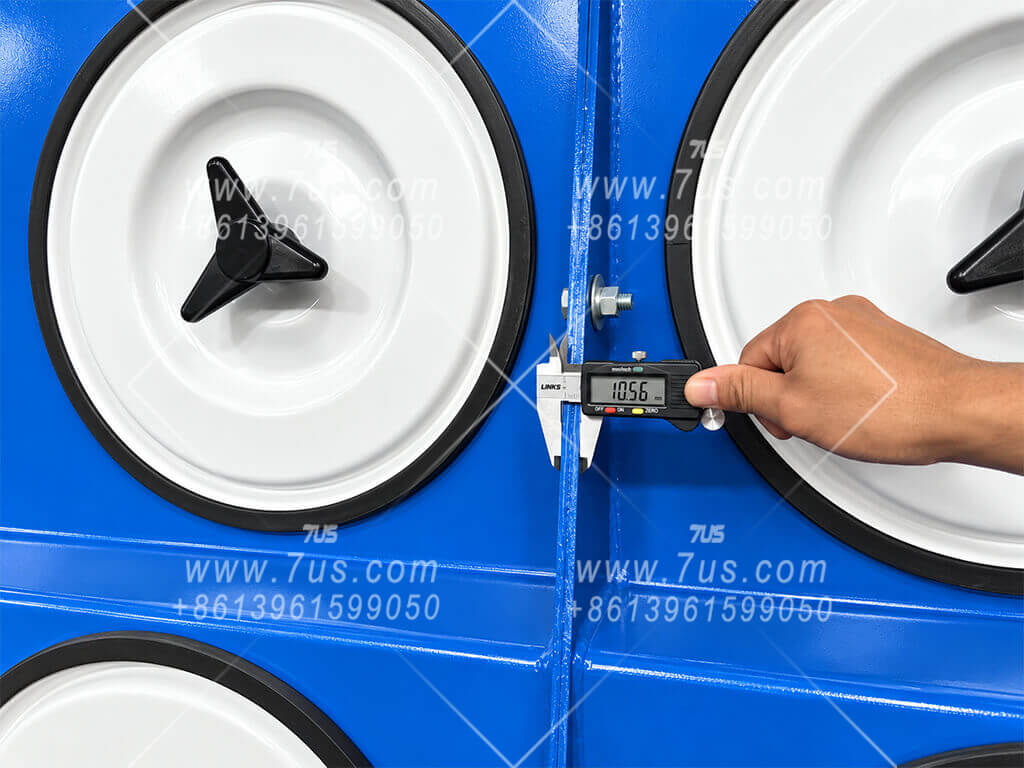
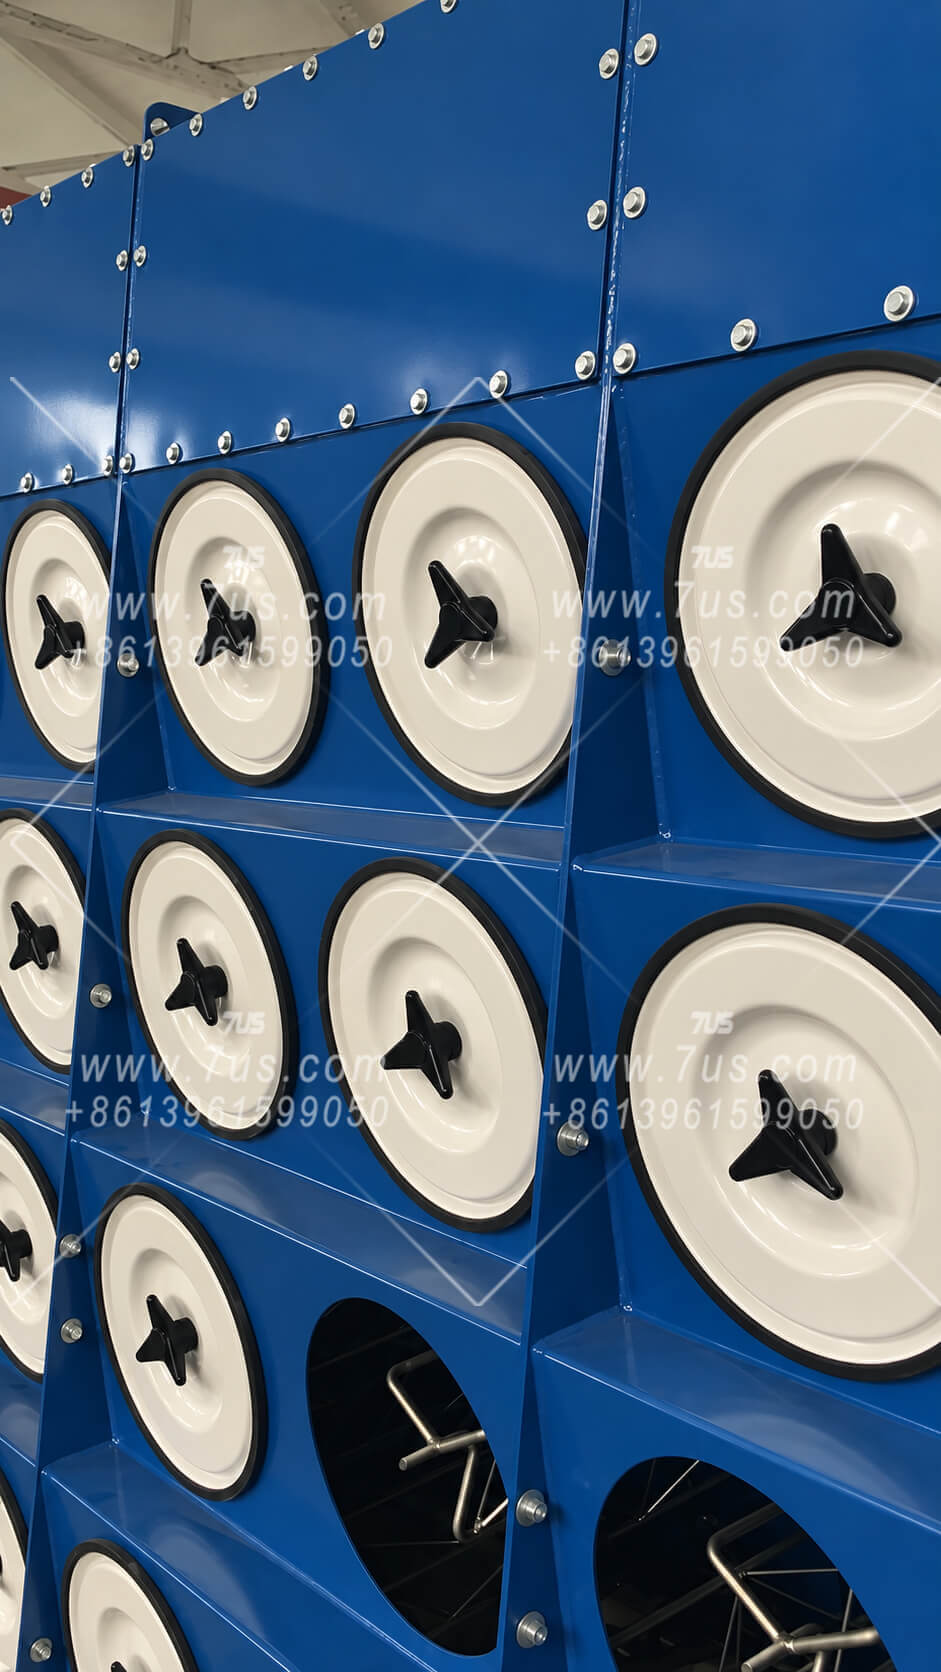
Close-up of 7US vertical module seam and fastening
Independent side plates form the structural connection zone
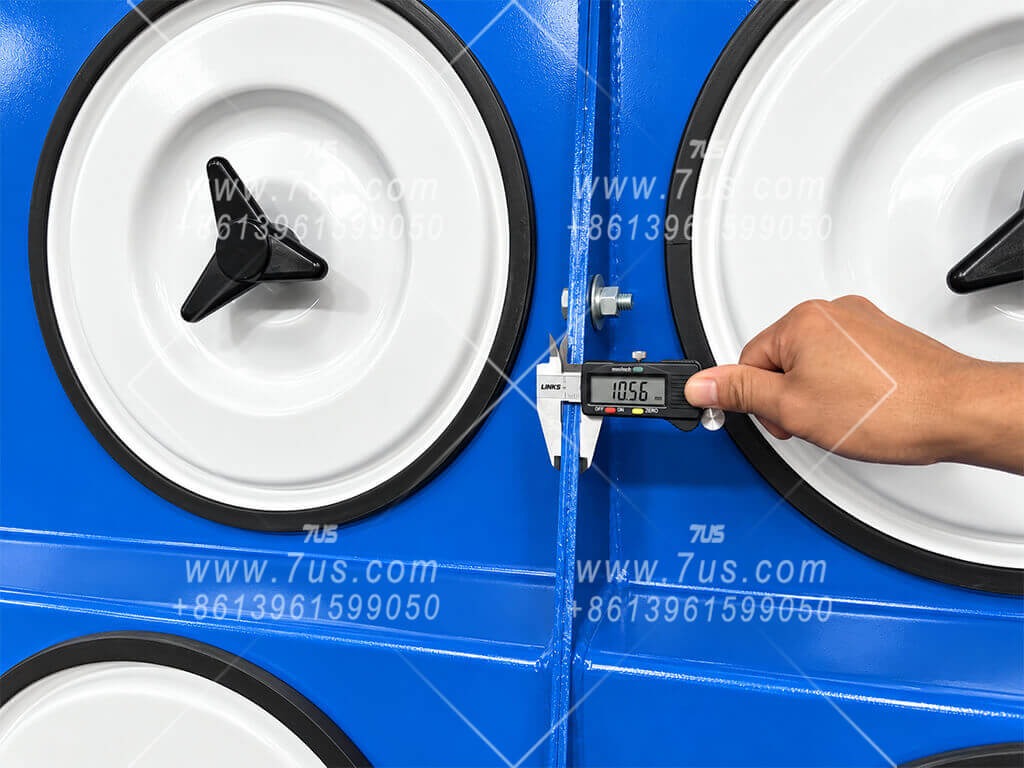
Caliper measurement at the assembled 7US module joint
Assembled module joint — directly measured

Each 7US module is fabricated as an independent structural unit with its own side plate. Before adjacent modules are bolted together, industrial structural sealant is applied continuously between the mating surfaces to create an air-tight interface. Bolts and nuts then provide the mechanical clamping force, forming a genuine sealed module-to-module structural joint.

Independent module side plates
Structural sealant applied between mating surfaces
Bolts and nuts provide mechanical clamping
Air-tight structural joint between modules
Sealed first, bolted second. The visible joint is structural — not decorative.
A true modular collector must address both structural strength and air-tightness. 7US modules are manufactured separately. During assembly, structural sealant is applied to the mating surfaces first to seal the interface; bolts and nuts are then tightened to provide the mechanical connection and clamping force. The modular concept therefore continues from factory fabrication through transport and final assembly.
05Manufacturing & Installation
Contents ↑
BUILT FOR ACCURACY

Manufacturing Details You Can See

A complete manufacturing process matters, but the details that affect fit, sealing and repeatability are easier to judge from real production evidence. The photographs below show how 7US controls fabrication, positioning, assembly and module fit-up in actual production.

01Laser Cutting
02CNC Bending
03Fixture Welding
04Trial Assembly
05Surface Preparation
06Powder Coating
07Final Assembly

Proof of Precision

Instead of relying only on specification text, these details show the actual fixtures, measurements, components and assembled modules used in production.
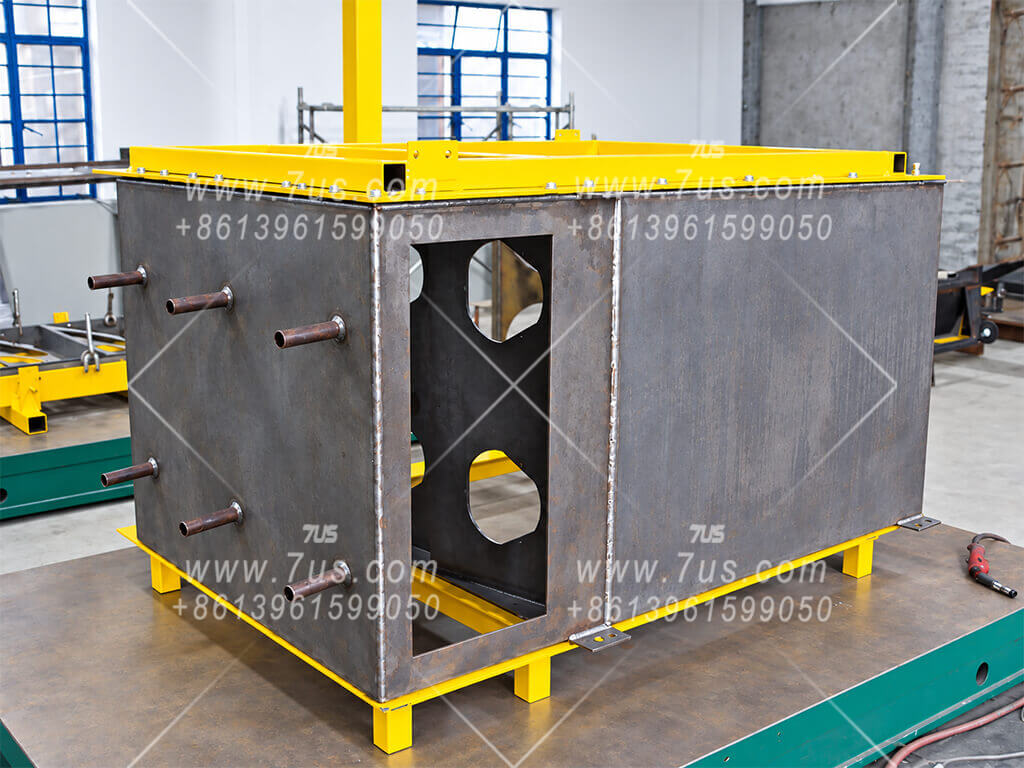
01

Fixture-Controlled Fabrication

Critical geometry is held during welding and checked again during trial assembly.
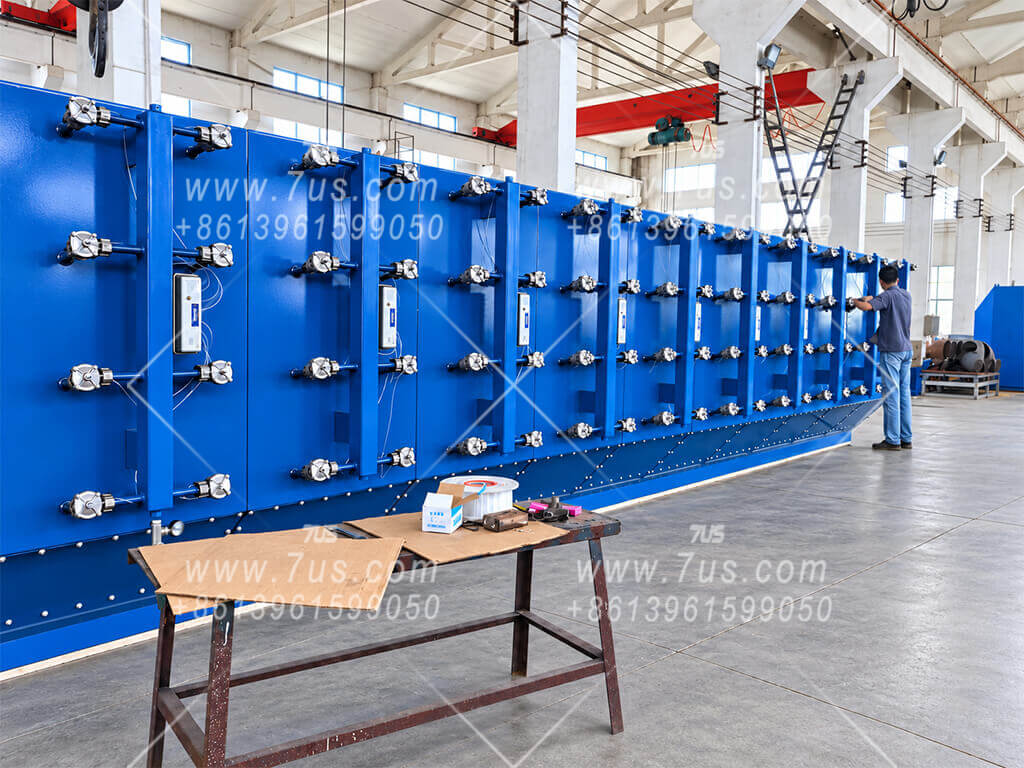
Welding fixture used for 7US cartridge dust collector cabinet fabrication
Dedicated welding fixture
Positioning and clamping detail during dust collector cabinet fabrication
Positioning & clamping detail
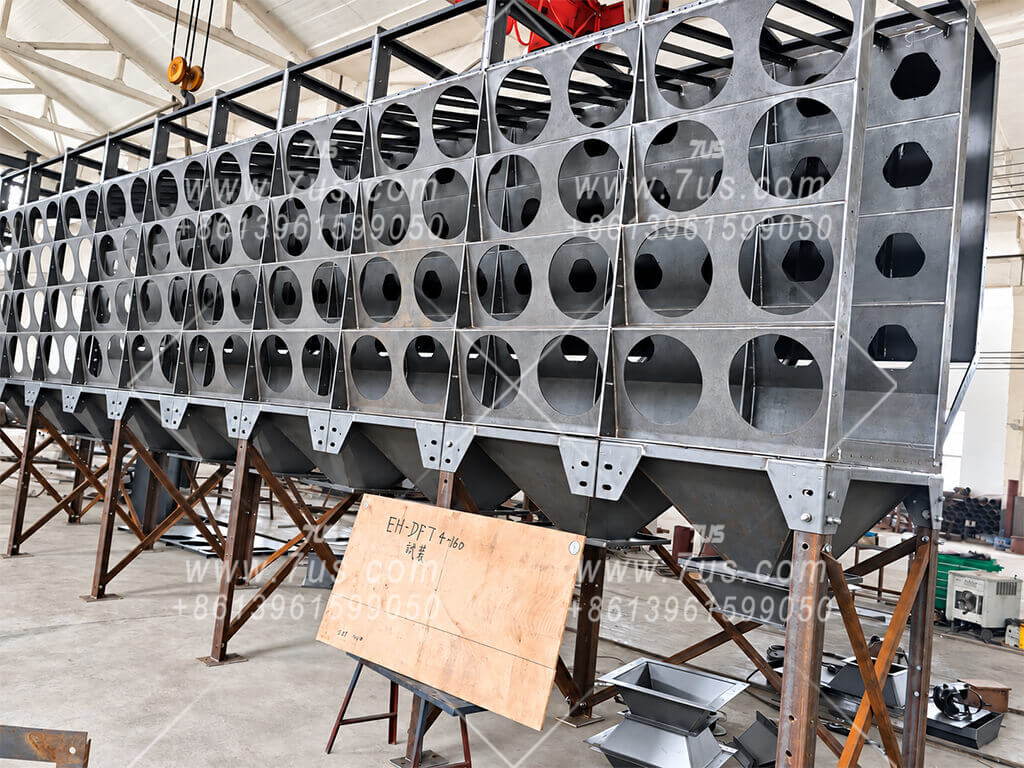
Uncoated modular cabinet trial assembly
Trial assembly before coating
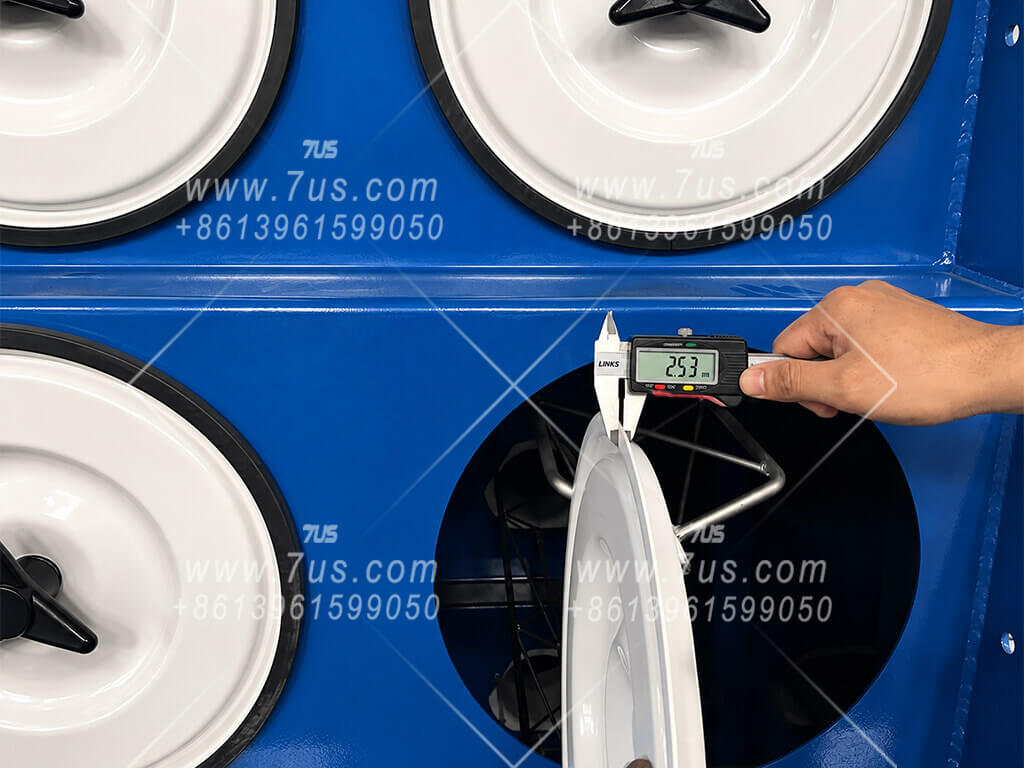
What customers can verify: the cabinet is not assembled only by visual alignment. Fixtures and pre-assembly are used to control repeatability before finishing.
02

Measured Construction Details

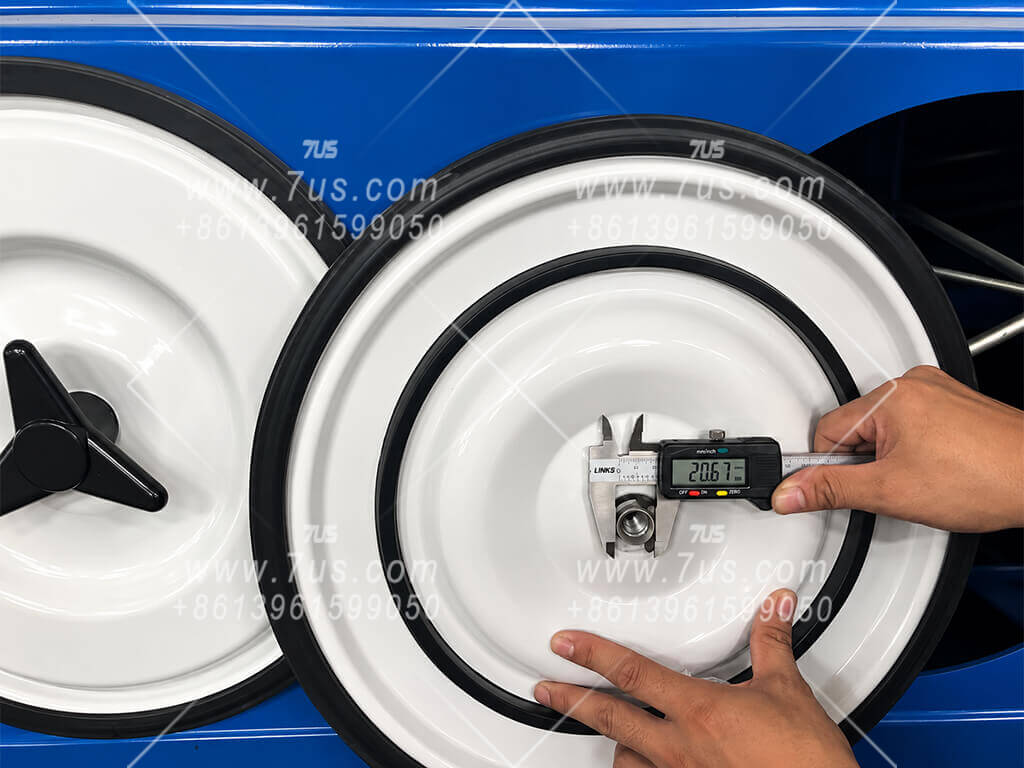
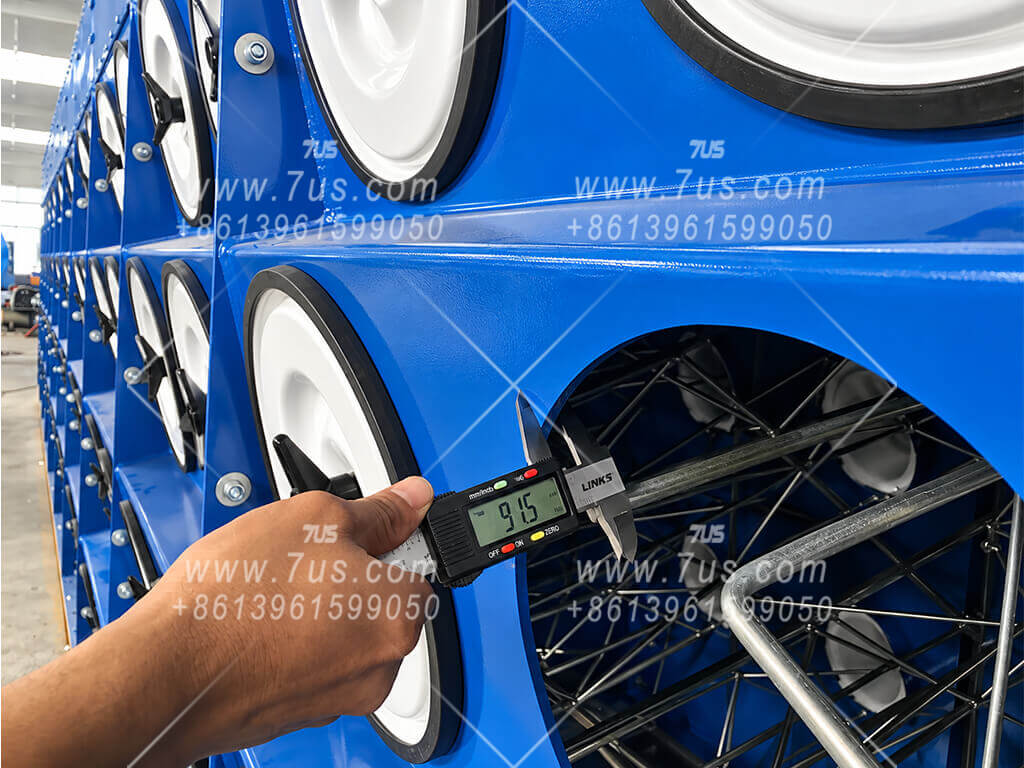
Real production measurements, hardware and grounding details are shown directly.
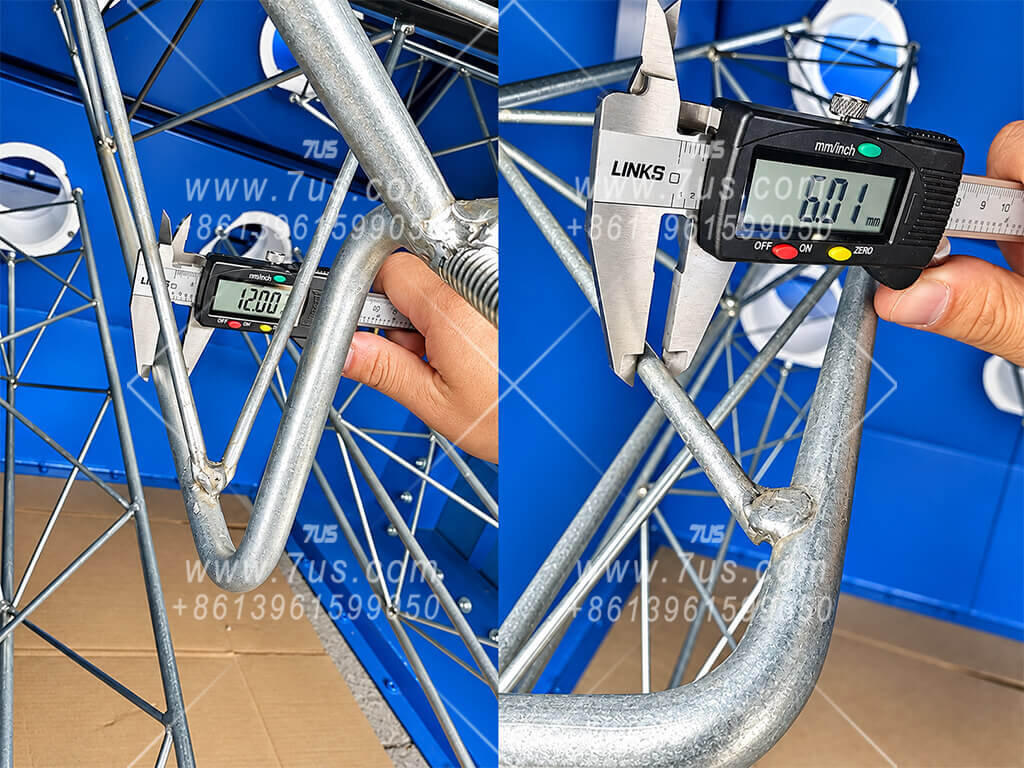
Filter support frame measurement
Filter-support frame members
Cover plate thickness measurement
Cover-plate thickness check
Three-lobe handle and threaded insert detail
Three-lobe handle & threaded insert
Curved plate thickness measurement
Curved structural plate
Module joint measurement
Module-joint build-up
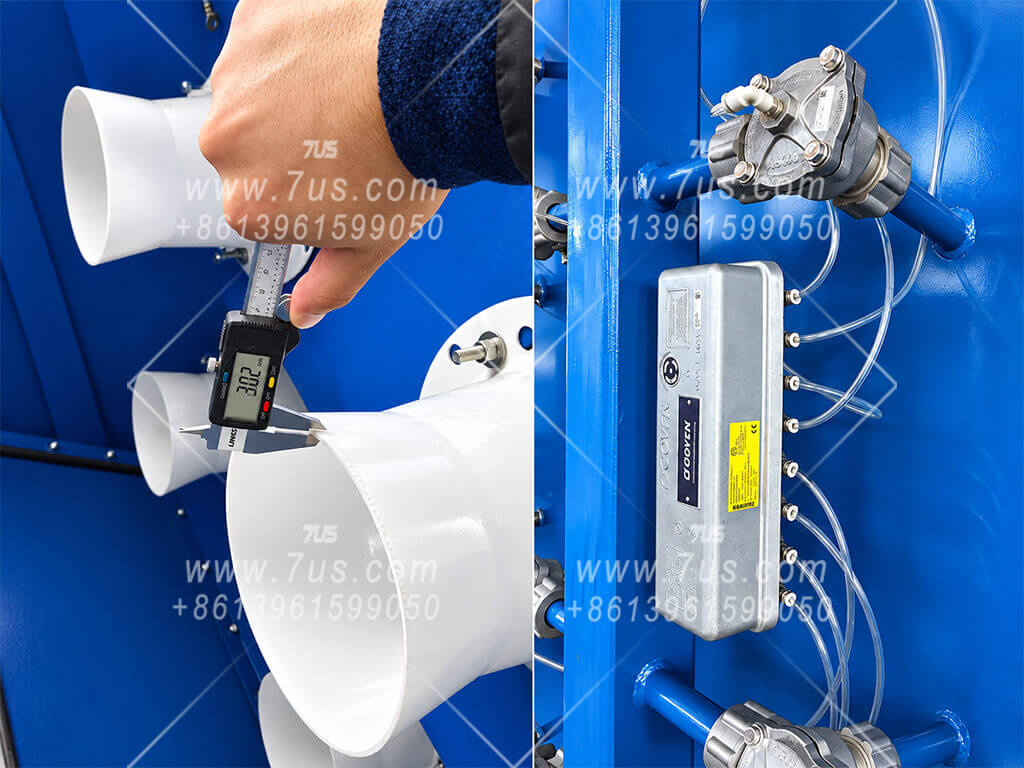
Venturi and pulse cleaning components
Venturi & pulse-cleaning hardware
White positioning jig for filter support installation
Positioning jig for support installation
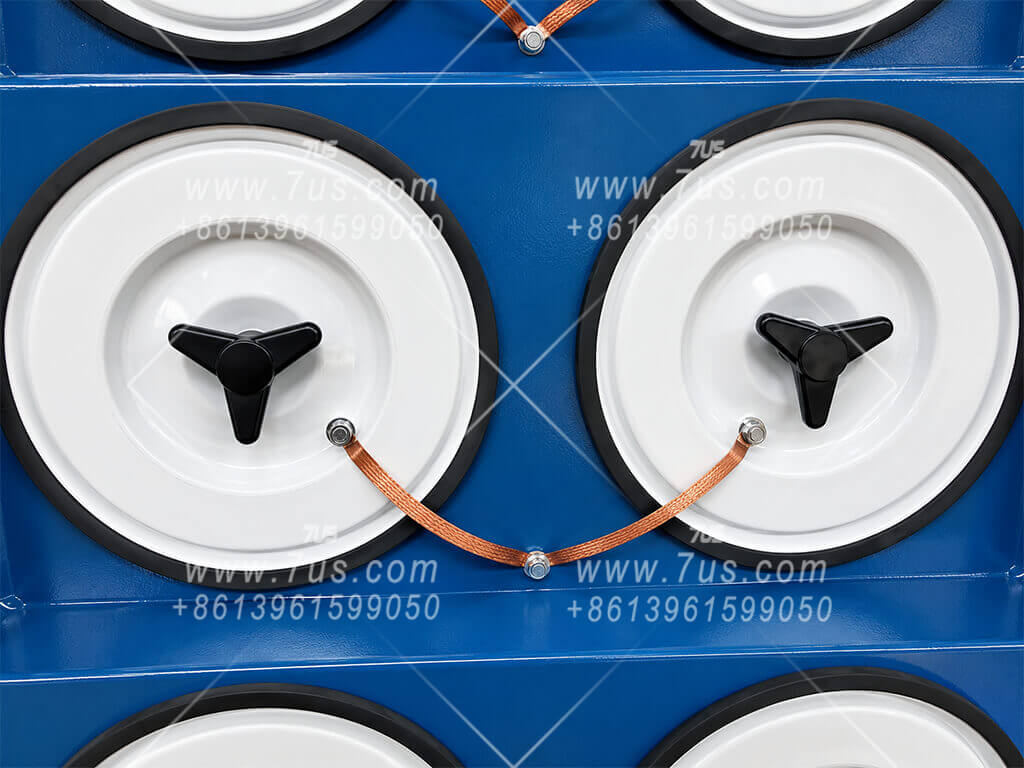
Copper grounding braid for static charge dissipation on the cartridge cover
Anti-static grounding braid
Eye-level evidence, not marketing claims: material thickness, frame construction, fastening, static-grounding and positioning methods can be inspected directly from production photographs.
03

Installation-Ready Duct Interfaces

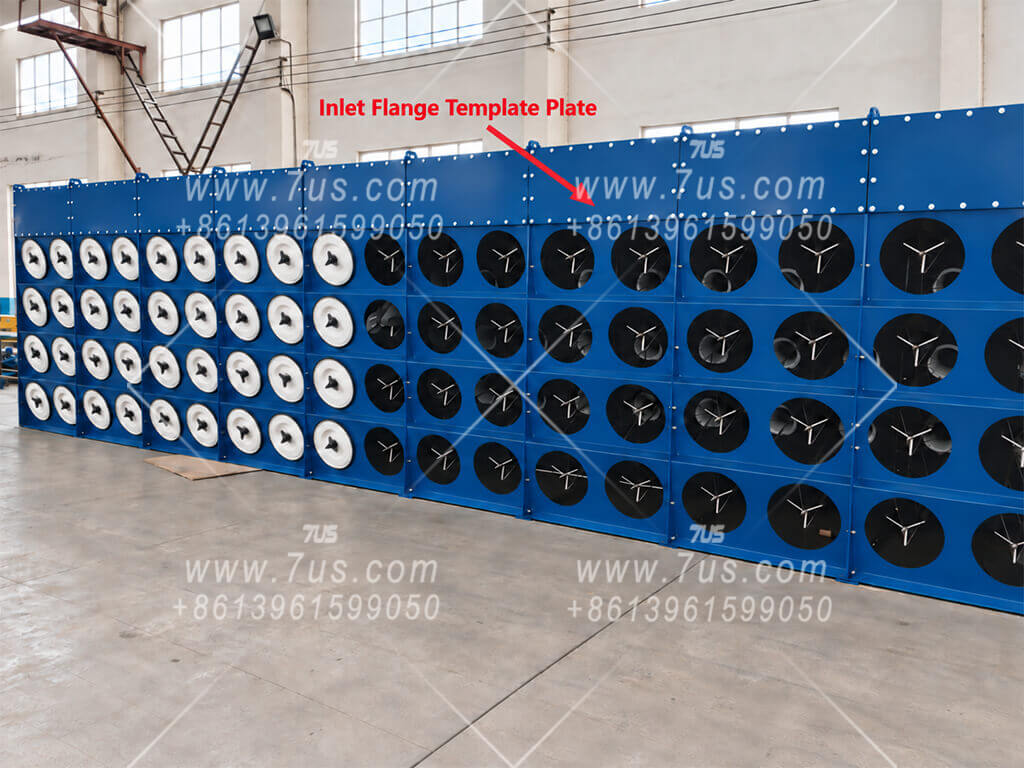
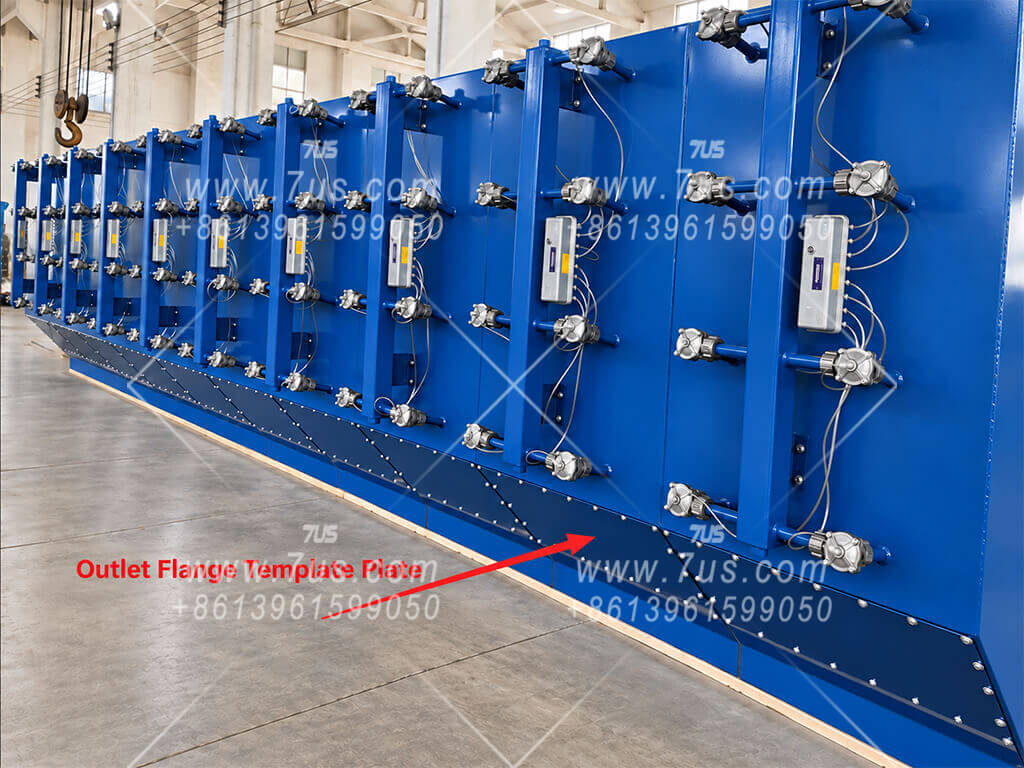
Removable inlet / outlet flange templates simplify matching ductwork fabrication.
Removable collector flange template
→Use as
fabrication pattern
Matching duct flange — same opening & bolt pattern
DESIGNED FOR EASIER INSTALLATION

Remove the Template. Build the Matching Flange.

7US inlet and outlet connections can be supplied with removable flange template plates. The template reproduces the actual collector opening size and bolt-hole pattern, so the duct fabricator can use the removed plate directly as the reference for the mating duct flange. This avoids repeated site measurement, redrawing and bolt-hole guesswork.
Exact Opening Size The duct flange follows the actual collector interface dimensions.
Exact Bolt Pattern Bolt-hole positions can be transferred directly from the template.
Faster Field Fit-Up Less measuring and fewer alignment surprises during duct connection.
A small manufacturing detail that can save significant installation time. The same concept can be used at both inlet and outlet interfaces.
Actual 7US dust collector showing removable inlet flange template plate
Inlet InterfaceFull-size removable flange template plate used as the duct fabrication pattern.
Actual 7US dust collector showing removable outlet flange template plate
Outlet InterfaceThe same removable-template concept applied to the clean-air outlet connection.
04

Independent Modular Construction

Upper and lower sections are fabricated separately, then assembled into one complete modular collector.
Front view of multiple assembled modules
Multiple modules — front view
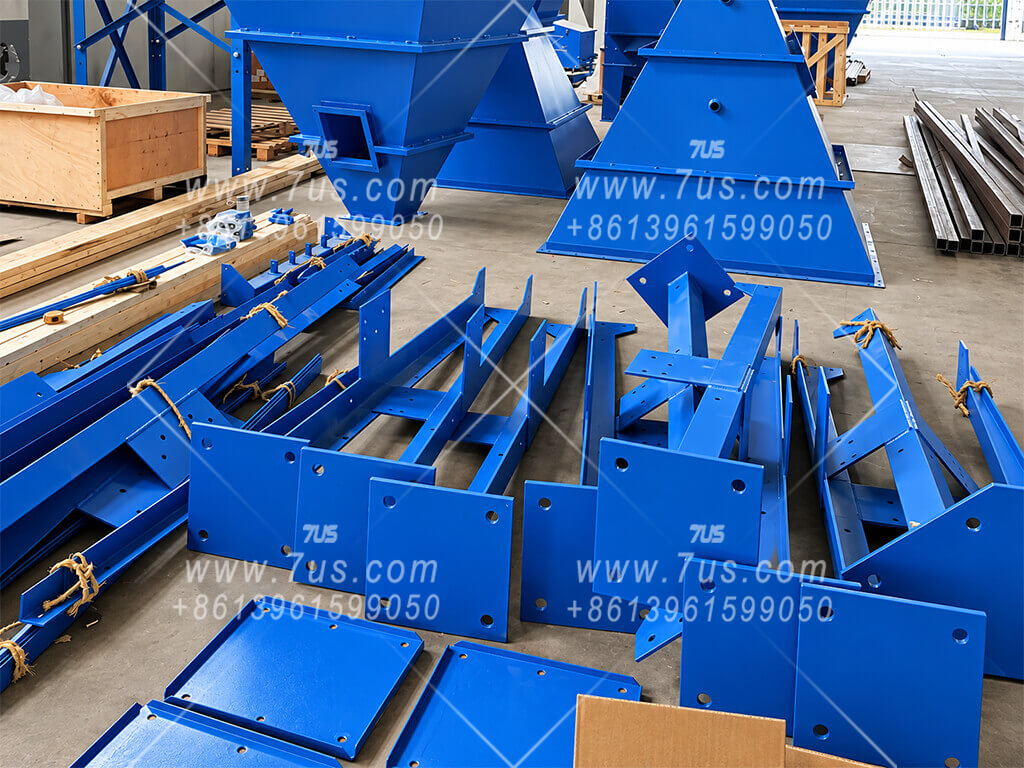
Powder-coated parts prepared for assembly
1 · Powder-coated parts ready for assembly
Upper housing section prepared as a separate assembly
2 · Upper housing section
Lower housing section prepared as a separate assembly
3 · Lower housing section
Complete collector after upper and lower sections are assembled together
4 · Complete unit after upper/lower assembly
The modular structure is visible through the assembly sequence. Powder-coated parts are prepared first; the upper housing and lower housing sections are built as separate assemblies, then aligned and bolted together to form the complete collector.
05

From Factory Trial Assembly to Site Installation

The same modular concept continues through inspection, transport and final erection.
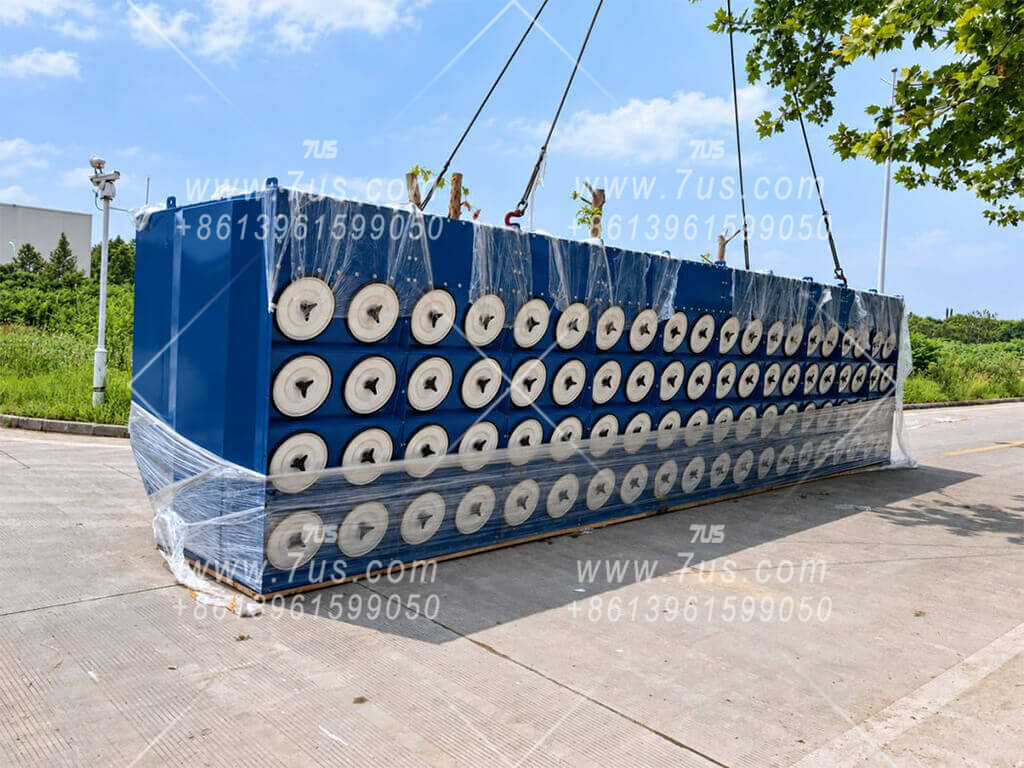
Factory trial assembly
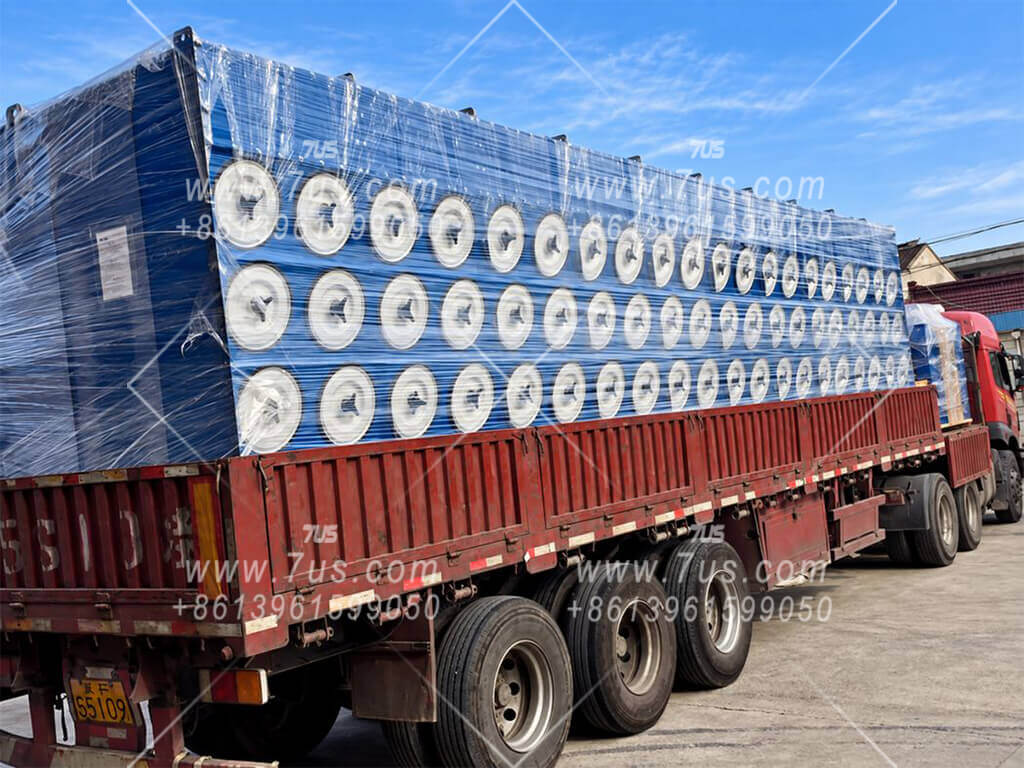
Large modular collector loaded for transport
Modular transport
Upper collector casing arrived at site
Upper casing at site
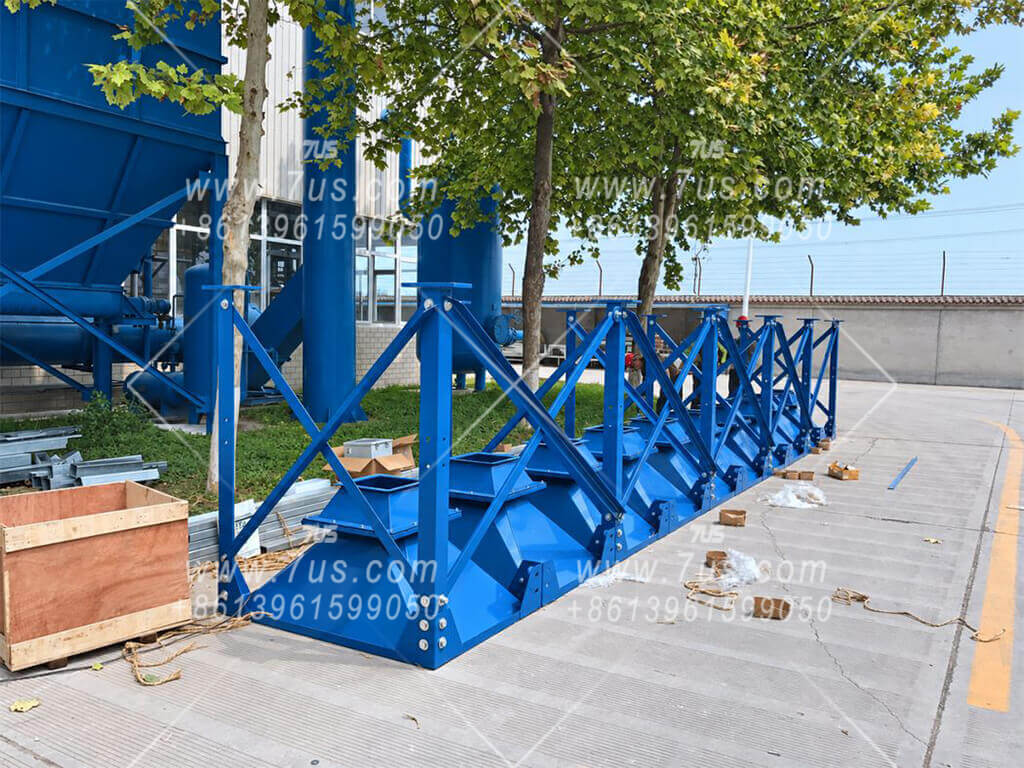
Lower collector structure at installation site
Lower structure positioned
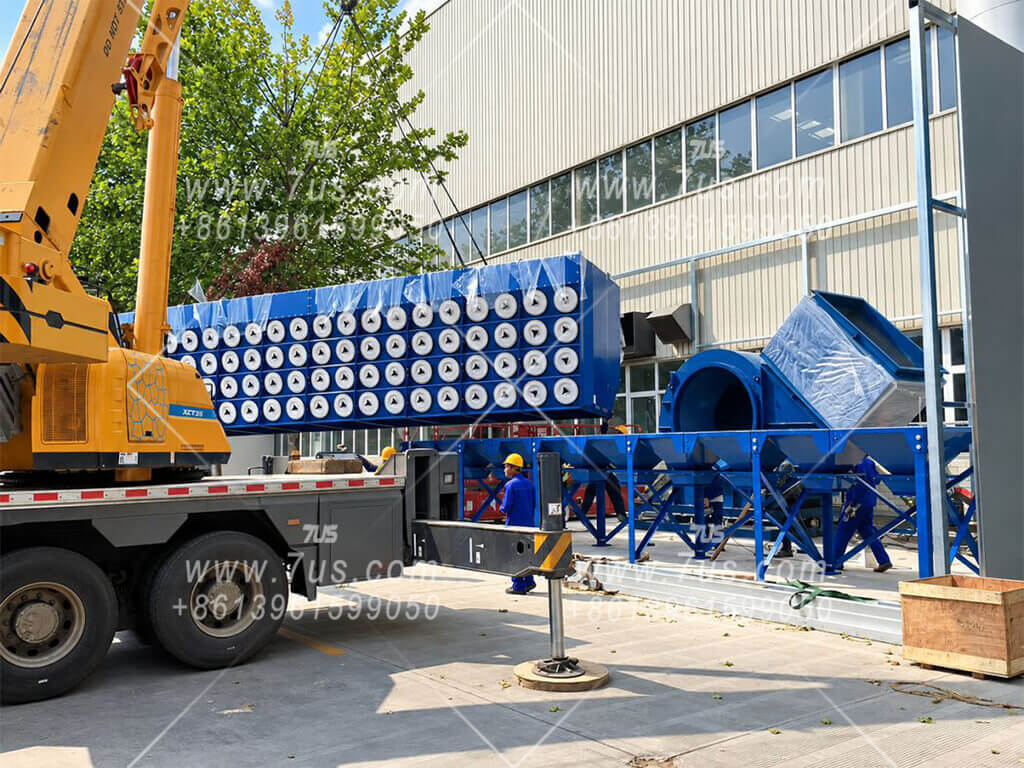
Crane assembling upper and lower collector modules
Crane-assisted assembly
Completed modular dust collector installation
Completed installation

Manufacturing Quality Should Be Visible

The goal of this section is not to claim quality with adjectives. It is to show the fixtures, measurements, construction details, trial assembly and finished installation so experienced buyers can judge the manufacturing standard for themselves.

Full process capability: laser cutting, CNC bending, welding, surface preparation and powder coating remain part of the complete process — but the details above are where manufacturing discipline becomes visible.

06Model Selection
Contents ↑

How to Select an EHCDT Downflow Collector

EHCDT selection is not simply “airflow equals one fixed model.” Start with the dust and filtration condition, then select the base module that best fits the available height, width and depth before building the complete system.

01Dust TypeFume, grinding dust, particulate and dust loading.
02Filter MediaPaper / cellulose or polyester.
03Filtration VelocitySet the design air-to-cloth ratio.
04Filter AreaCalculate the effective area required.
05Site SpaceCheck height, width, depth and access.
06Base ModuleSelect the suitable standard geometry.
07Complete SystemCombine modules for the final duty.
Core principle: choose the filtration condition first, then choose the module. Cartridge quantity alone does not determine collector capacity.
06.1

Selection Basics

Filter-media characteristics together with pleat quantity, pleat depth and pleat arrangement determine the effective filter area of each cartridge, while the selected design filtration velocity determines the total filter area required for the target airflow.

FINE FUME / LOWER PARTICULATE LOADING

Paper / Cellulose Media

≈20 m²per cartridge

Because paper / cellulose media can be pleated more densely within the same outside cartridge size, a larger effective filter area can be achieved in the same volume. The denser pleat arrangement, however, also increases airflow resistance, so the recommended design filtration velocity is lower than for polyester media. This configuration is well suited to welding fumes and similar fine-fume duties.

  • Same outside size as the polyester option
  • Larger effective filter area
  • Can reduce module quantity for suitable fume duties
  • Recommended design filtration velocity: generally ≤0.8 m/min
HIGHER PARTICULATE LOADING

Polyester Media

≈10 m²per cartridge

Wider pleat spacing is better suited to grinding dust and higher particulate loading, where dense pleats can make pulse-cleaning and dust shedding more difficult.

  • Same outside size as the paper / cellulose option
  • More open pleat spacing for particulate release
  • Preferred for grinding and higher dust-loading duties
  • Recommended design filtration velocity: generally ≤1.1 m/min
The filter-area and filtration-velocity values above are preliminary selection guidance for this product family. For high dust loading, stricter emission targets, continuous heavy-duty operation or other special conditions, a lower design filtration velocity may be appropriate.
EHCDT4-32 / Polyester 32 cartridges × ≈10 m²
≈320 m² total filter area
vs.
EHCDT4-32 / Paper-Cellulose 32 cartridges × ≈20 m²
≈640 m² total filter area
View the EHCDT4-32 airflow example and design note

For an EHCDT4-32 fitted with 32 cartridges, airflow should be evaluated from both total effective filter area and the recommended design filtration velocity. With polyester media, using approximately 10 m² per cartridge gives about 320 m² total filter area. At the recommended upper design velocity of 1.1 m/min, the calculated airflow is about 21,120 m³/h; around 20,000 m³/h is a practical preliminary selection example. With paper / cellulose media, using approximately 20 m² per cartridge gives about 640 m² total filter area. At the recommended upper design velocity of 0.8 m/min, the calculated airflow is about 30,720 m³/h; around 30,000 m³/h is a practical preliminary selection example. A larger filter area therefore does not mean that airflow can increase in the same proportion, because the allowable design filtration velocity is different for the two media types.

These comparisons assume that each filter medium is suitable for the actual dust duty. Changing to paper / cellulose media does not automatically justify increasing airflow in every application. Final selection should also consider the actual effective filter area, dust characteristics and concentration, target emissions, cleaning conditions, operating hours and overall system resistance.
06.2

Choose the Base Module

The model code describes the basic geometry, while height, width and depth can be adjusted to fit the real installation space.

EHCDT 4 – 16

Depth Can Also Change

The same family can use one cartridge or two cartridges in series on each support frame.

Single-Cartridge DepthExamples: EHCDT2-4D and EHCDT3-6D
1 support frame = 1 cartridge. Used to reduce collector depth.
Dual-Cartridge DepthExample: EHCDT3-12
1 support frame = 2 cartridges in series. More filter area in the depth direction.
HEIGHT AVAILABLE

EHCDT4-24

One complete 4-level module provides all 24 cartridges in the most compact horizontal arrangement.

Base modules1 × EHCDT4-24Levels4Total cartridges24
LOWER HEIGHT

EHCDT3-24

Two EHCDT3-12 modules provide the same 24 cartridges when 4 levels are too high.

Base modules2 × EHCDT3-12Levels3Total cartridges24
MINIMUM HEIGHT

EHCDT2-24

Three EHCDT2-8 modules spread the same 24 cartridges horizontally where height is even more restricted.

Base modules3 × EHCDT2-8Levels2Total cartridges24
Selection is three-dimensional: height, width and depth can be traded against one another while keeping the required filter area.
06.3

Standard Modules & Scaling

Choose a standard base module, then combine identical or compatible modules to build the complete collector.

ModelLevelsCartridgesDepth ArrangementReference AirflowSize L × W × H (mm)Pulse ValvesN.W.
EHCDT2-4D24Single-cartridge depthTo be confirmedTo be confirmedTo be confirmedTo be confirmed
EHCDT3-6D36Single-cartridge depth3,750 m³/h1016 × 1434 × 34926 × DN200.579 T
EHCDT2-828Dual-cartridge depth5,000 m³/h1016 × 2162 × 32482 × DN250.841 T
EHCDT3-12312Dual-cartridge depth7,500 m³/h1016 × 2162 × 36756 × DN250.953 T
EHCDT3-18318Extended-width / dual-depth11,250 m³/h1523 × 2162 × 36759 × DN251.710 T
EHCDT4-16416Dual-cartridge depth10,000 m³/h1016 × 2162 × 41408 × DN251.164 T
EHCDT4-24424Extended-width / dual-depth15,000 m³/h1523 × 2162 × 414012 × DN251.481 T
Reference airflow is for preliminary selection only. Filter-media characteristics together with pleat quantity, pleat depth and pleat arrangement determine the effective filter area of each cartridge, while the selected design filtration velocity determines the total filter area required for the final airflow.
4-LEVEL COMPATIBLE FAMILY

EHCDT4-16 + EHCDT4-24

EHCDT4-24 is a complete standard module with the same 4-level family and 1.5× the cartridge quantity of EHCDT4-16. The two sizes can be combined side by side.

3-LEVEL COMPATIBLE FAMILY

EHCDT3-12 + EHCDT3-18

The same principle applies to the 3-level family. Standard-width and extended-width modules can be used individually or combined.

STEP 1Select the Base Module

Match dust duty, filter area and site envelope.

STEP 2Set Module Quantity

Add identical or compatible modules to reach capacity.

STEP 3Confirm Overall Layout

Check width, hoppers, duct interfaces and access.

STEP 4Finalize the Project Model

Confirm fan pressure, discharge, controls and drawings.

EXAMPLE

EHCDT4-16 Modular Series

One commonly used example only. Other base modules can be combined according to the same modular principle.

EHCDT4-161 module · 10,000 m³/h
EHCDT4-322 modules · 20,000 m³/h
EHCDT4-483 modules · 30,000 m³/h
EHCDT4-644 modules · 40,000 m³/h
EHCDT4-805 modules · 50,000 m³/h
View full EHCDT4-16 combination table
Base ModulesCombined ModelReference AirflowOverall Size L × W × H (mm)CartridgesPulse ValvesN.W.
1EHCDT4-1610,000 m³/h1016 × 2162 × 4140168 × DN251.164 T
2EHCDT4-3220,000 m³/h2032 × 2162 × 41403216 × DN252.005 T
3EHCDT4-4830,000 m³/h3048 × 2162 × 41404824 × DN252.882 T
4EHCDT4-6440,000 m³/h4064 × 2162 × 41406432 × DN253.661 T
5EHCDT4-8050,000 m³/h5080 × 2162 × 41408040 × DN254.520 T
6EHCDT4-9660,000 m³/h6096 × 2162 × 41409648 × DN255.357 T
7EHCDT4-11270,000 m³/h7112 × 2162 × 414011256 × DN256.394 T
8EHCDT4-12880,000 m³/h8128 × 2162 × 414012864 × DN257.230 T
9EHCDT4-14490,000 m³/h9144 × 2162 × 414014472 × DN257.867 T
10EHCDT4-160100,000 m³/h10160 × 2162 × 414016080 × DN258.704 T
Reference basis: the airflow values in this combination table are based on polyester cartridges at approximately 10 m² per cartridge and a design filtration velocity of about 1.04 m/min, for preliminary selection only. When paper / cellulose media or another effective filter-area configuration is used, airflow should be recalculated using the corresponding recommended design filtration velocity. Final airflow, overall dimensions and weight should still be confirmed for the actual dust duty and project-specific arrangement.
07 EHCDP Horizontal Series
Contents ↑
HORIZONTAL CARTRIDGE ARRANGEMENT

EHCDP Horizontal Cartridge Dust Collector

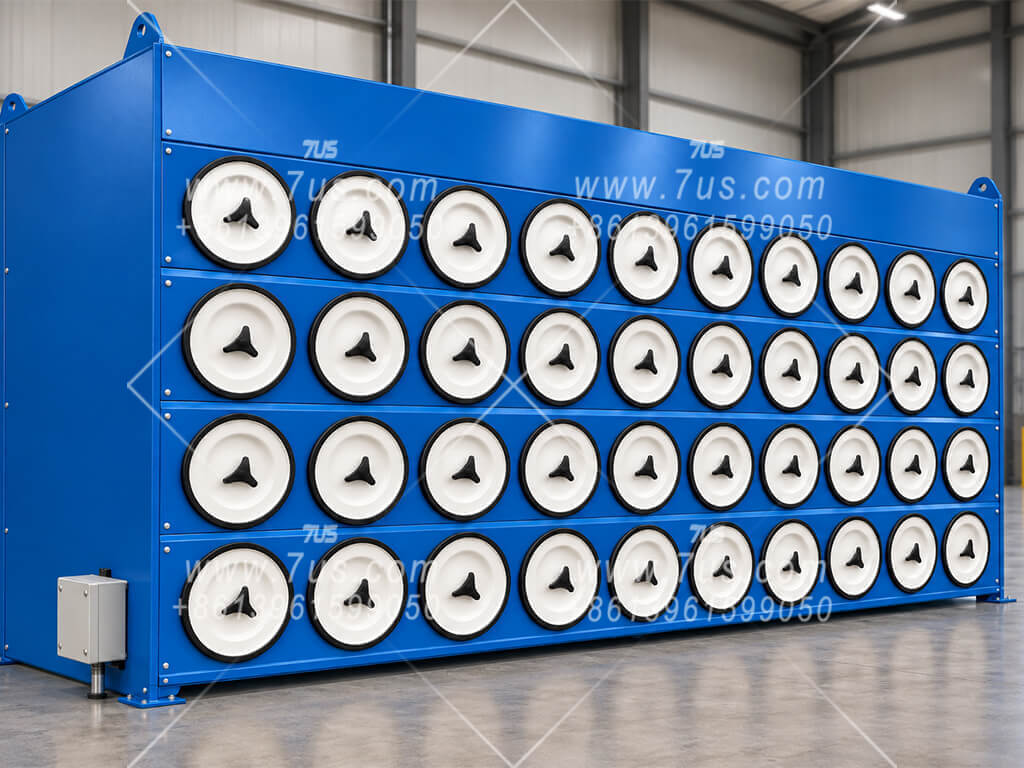
EHCDP uses the same modular collector concept and the same basic filtration / pulse-cleaning logic shown above, but the filter cartridges are installed horizontally instead of at an inclined angle. The horizontal family also extends to a 5-level configuration, providing another way to increase cartridge quantity where the available installation height allows it.
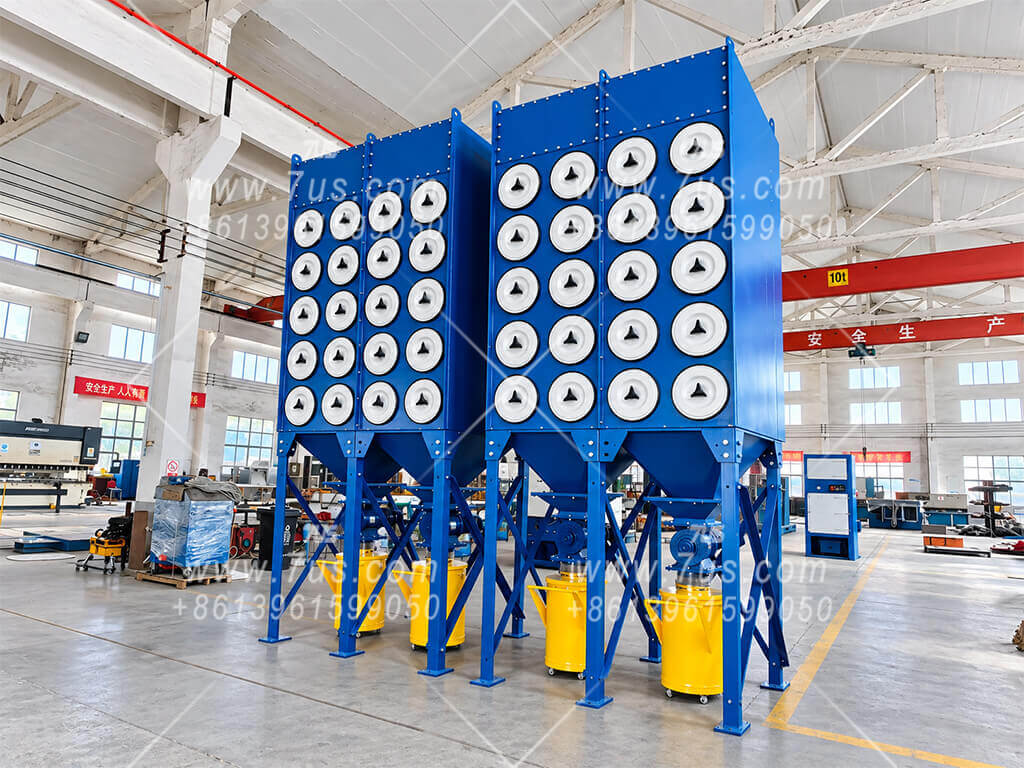
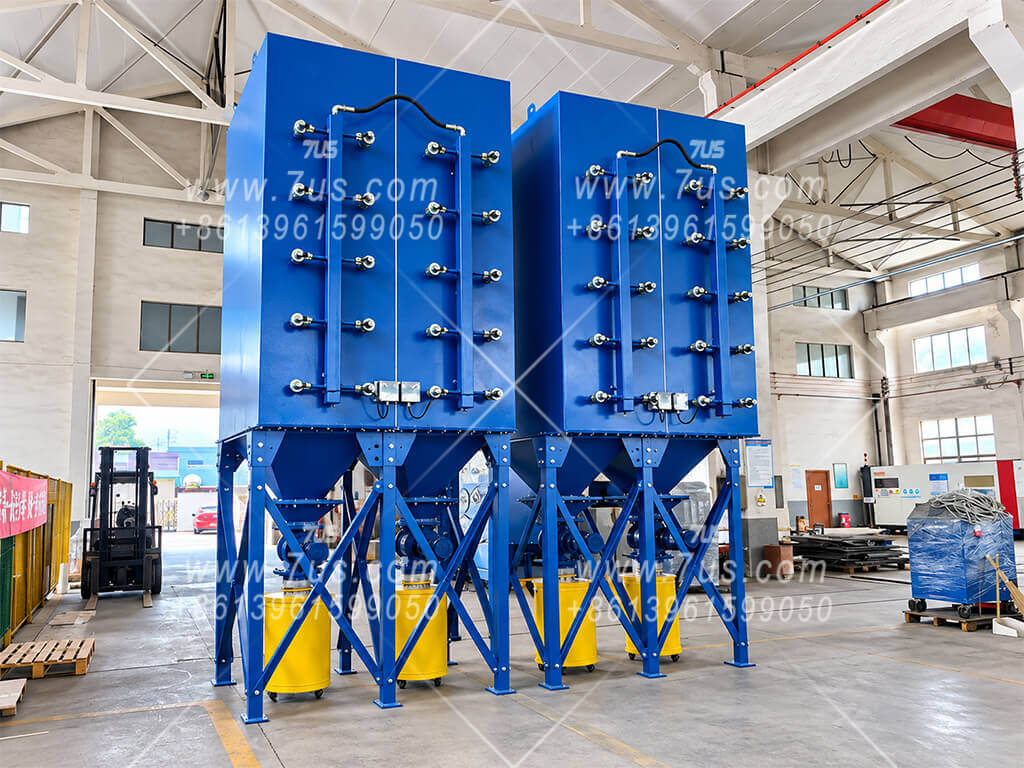
Shared platform, different cartridge orientation. Cartridge sealing, true modular construction, removable duct-interface templates and the manufacturing controls shown in Chapters 03–05 also apply to the EHCDP family unless a project-specific configuration is stated.
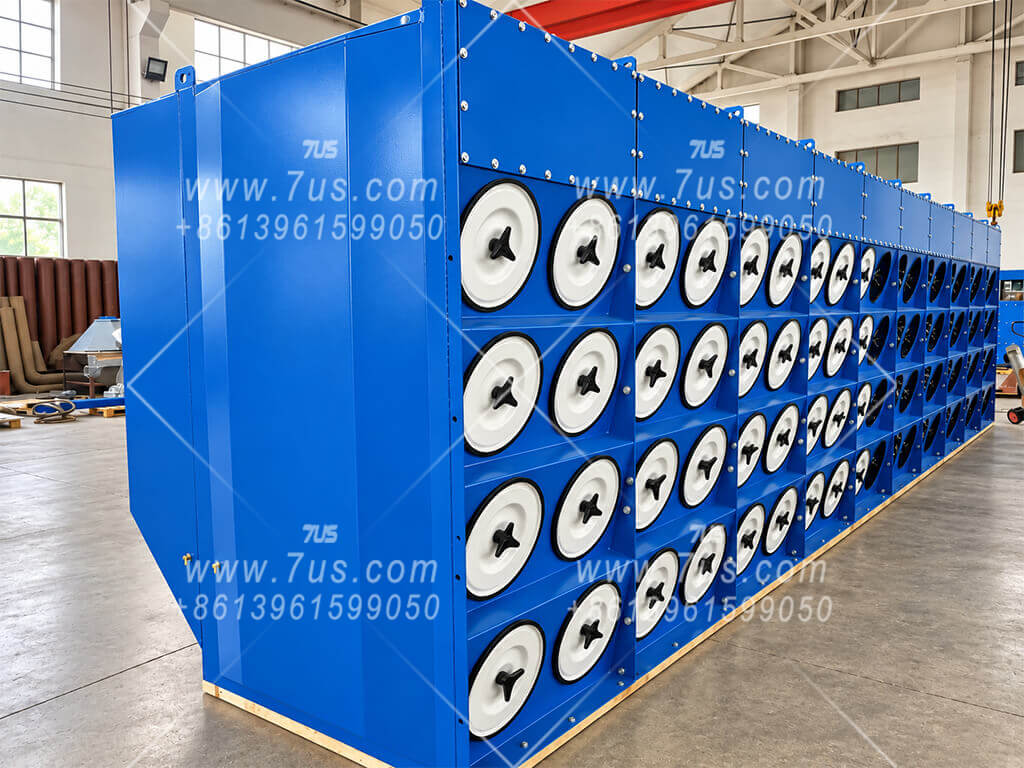
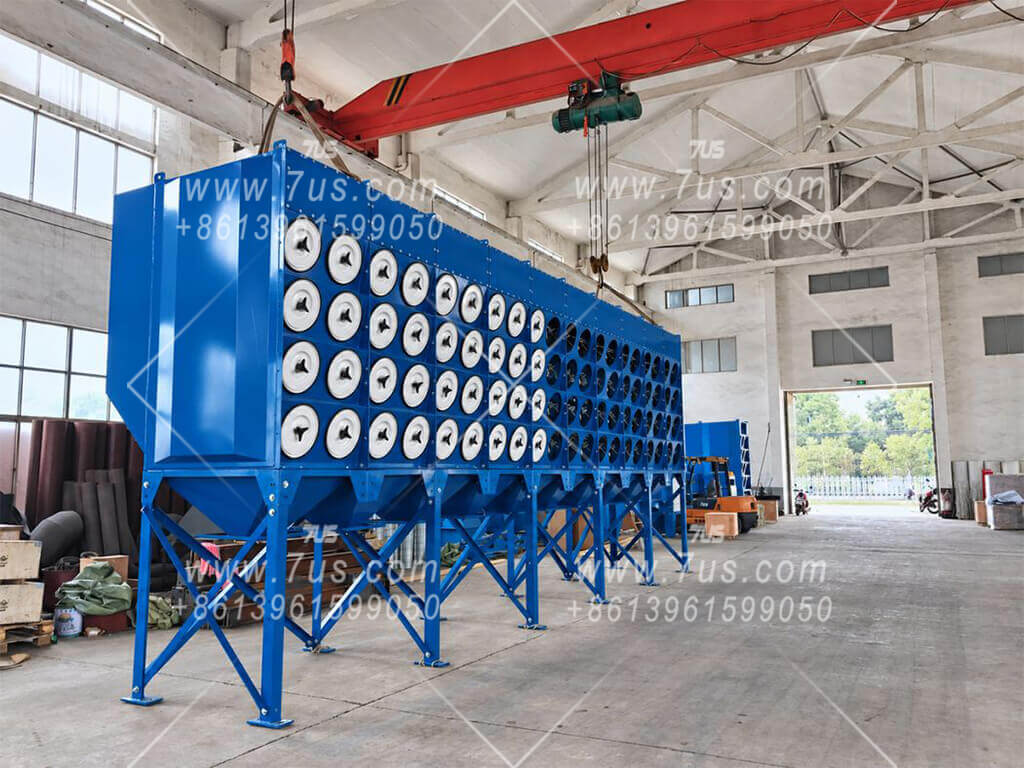
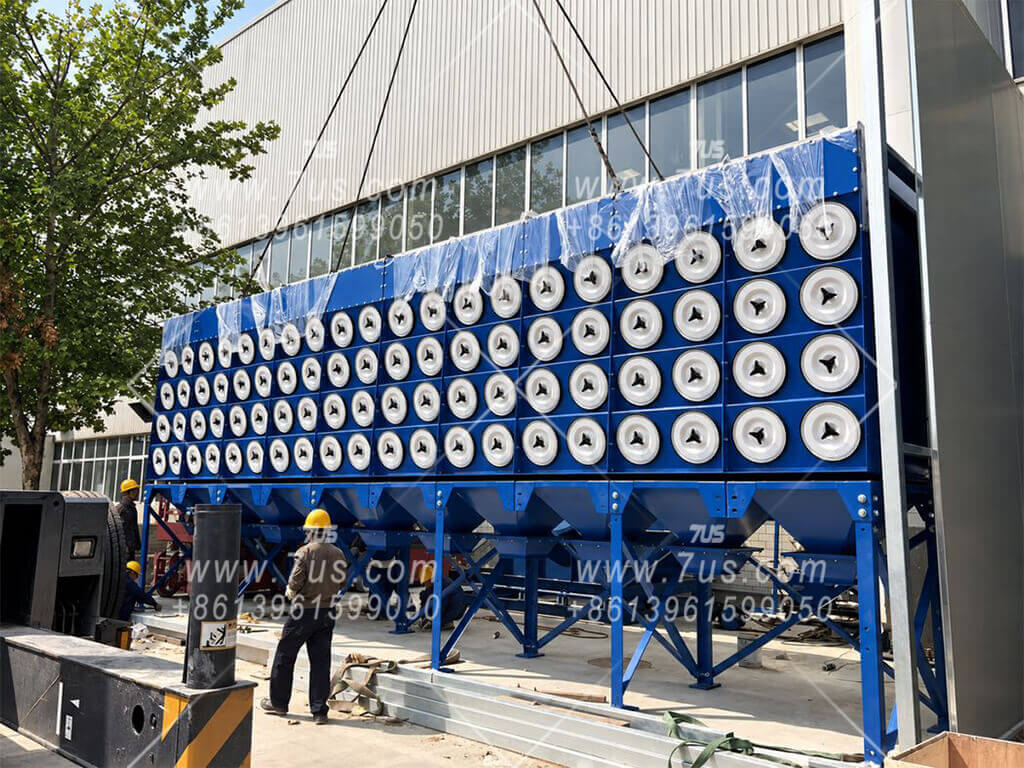
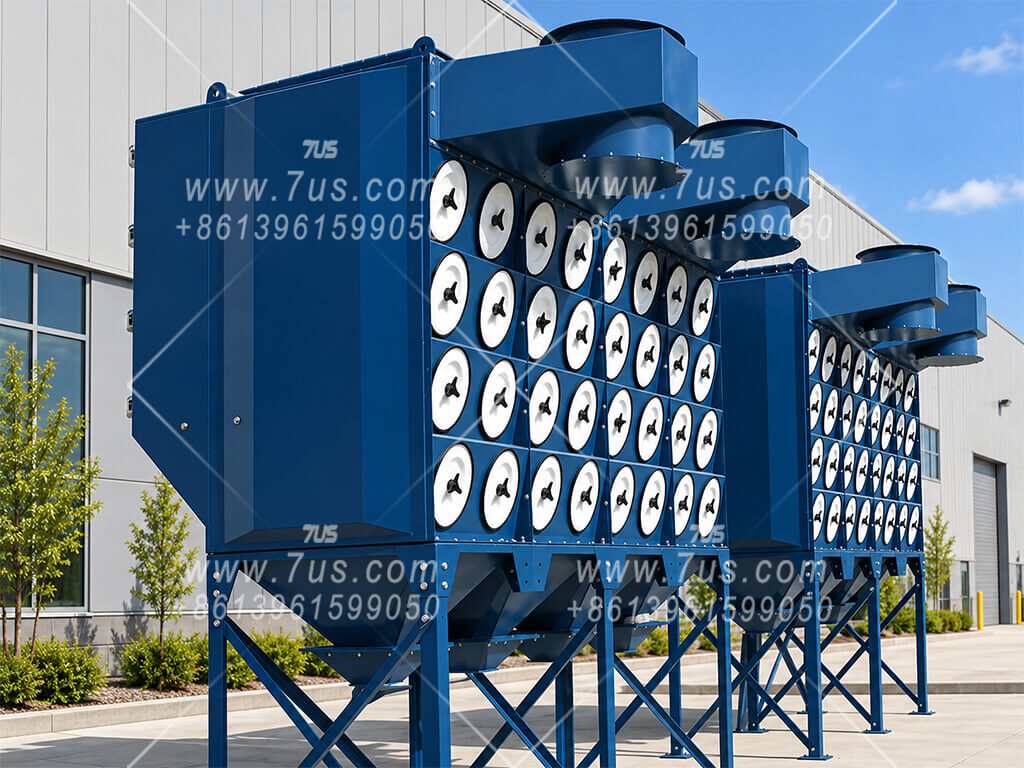
EHCDP horizontal cartridge dust collector front view
Front ViewActual EHCDP horizontal-cartridge modular collector.
EHCDP horizontal cartridge dust collector rear view
Rear ViewRear-side structure of the same horizontal-cartridge platform.
CARTRIDGE ORIENTATION Horizontal Side Insertion Cartridges remain level and are accessed from the service side.
STANDARD CARTRIDGE Ø352 × 660 mm The same standard outside cartridge size used in the EHCDT family.
ADDITIONAL HEIGHT OPTION 2 / 3 / 4 / 5 Levels The 5-level arrangement increases cartridge quantity without adding another module across the floor width.
CAPACITY EXPANSION Modular Combination Base modules can be combined side by side according to required filter area and site layout.

EHCDP Standard Module Selection

The model code identifies the filter levels and total cartridge quantity. Final airflow is confirmed from filter media, total effective filter area and the design filtration velocity for the actual dust — not from cartridge quantity alone.

Model Filter Levels Cartridges Cartridge Size Paper / Cellulose Area* Polyester Area* Arrangement
EHCDP2-424Ø352 × 660 mm≈ 80 m²≈ 40 m²Compact-width module
EHCDP2-828Ø352 × 660 mm≈ 160 m²≈ 80 m²Standard-width module
EHCDP3-636Ø352 × 660 mm≈ 120 m²≈ 60 m²Compact-width module
EHCDP3-12312Ø352 × 660 mm≈ 240 m²≈ 120 m²Standard-width module
EHCDP3-18318Ø352 × 660 mm≈ 360 m²≈ 180 m²Extended-width module
EHCDP4-16416Ø352 × 660 mm≈ 320 m²≈ 160 m²Standard-width module
EHCDP4-24424Ø352 × 660 mm≈ 480 m²≈ 240 m²Extended-width module
EHCDP5-20 5 Level520Ø352 × 660 mm≈ 400 m²≈ 200 m²Standard-width / taller module
EHCDP5-30 5 Level530Ø352 × 660 mm≈ 600 m²≈ 300 m²Extended-width / taller module
SELECTION PRINCIPLE Airflow = Total Filter Area × Design Filtration Velocity × 60

This keeps EHCDP selection consistent with the engineering logic used for EHCDT. A model number describes the module geometry; the acceptable airflow still depends on dust loading, filter media and the filtration velocity selected for the application.

TYPICAL AREA FOR PRELIMINARY SELECTION

Cartridges with the same outside dimensions can have different effective filtration areas because the pleat construction is different.

≈20 m² / cartridgePaper / cellulose media
≈10 m² / cartridgePolyester media

Example: EHCDP3-12 Modular Scaling

One 3-level base module can be repeated horizontally. The same modular principle also applies to compatible 2-, 4- and 5-level families.

EHCDP3-121 module · 12 cartridges
EHCDP3-242 modules · 24 cartridges
EHCDP3-363 modules · 36 cartridges
EHCDP3-484 modules · 48 cartridges
EHCDP3-605 modules · 60 cartridges
* Filter areas above use the same simplified preliminary-selection basis used in Chapter 06: approximately 20 m² per paper / cellulose cartridge and 10 m² per polyester cartridge. Final cartridge construction, media specification, dimensions and project airflow are confirmed before order.
08 System Options
Contents ↑
CONFIGURE THE COLLECTOR AROUND THE PROJECT

Available System Options

The downflow cartridge dust collector body can be configured around the actual dust load, discharge method, electrical standard, safety requirements and final filtration target. The options below can be selected individually or combined as part of a project-specific system configuration.

01 · FILTER CARTRIDGES

Filter Media Options

Select the basic media first, then add surface or safety functions according to the dust.

  • Cellulose / paper filter cartridges
  • Polyester filter cartridges
  • PTFE membrane optional
  • Flame-retardant option
  • Antistatic option
02 · MATERIAL & CONSTRUCTION

Collector Material & Structural Customization

The collector body can be manufactured in different materials and structural specifications to suit corrosion conditions, process requirements and customer standards.

  • Q235 carbon steel
  • SS304 stainless steel
  • SS316L stainless steel
  • Customer-specified coating color
  • Plate thickness can be customized for special service conditions
  • Reinforcement and structural strengthening can be customized as required
03 · HOPPER CONFIGURATIONS

Independent or Boat-Type Hopper

Independent Hopper
  • Low-profile hopper for lower dust loading
  • High-capacity hopper for higher dust loading
Boat-Type Hopper
  • One common large hopper can serve multiple collector modules
04 · DUST DISCHARGE

Discharge Valve & Screw Conveyor

  • Manual slide gate
  • Manual butterfly valve
  • Motorized rotary airlock valve
  • Screw conveyor available for multi-module collectors
05 · PULSE CLEANING

Pulse-Jet Cleaning System

  • Pneumatic pilot-operated valves + centralized solenoid valve box
  • Integrated solenoid-operated pulse valves
  • Pulse interval and duration adjustable by pulse controller or PLC
  • Valve and control component brands can be specified
06 · FAN & ELECTRICAL CONTROL

Fan, Motor & Control Cabinet

Fan / Motor
  • Fan brand and motor brand can be specified
  • Voltage and 50 / 60 Hz frequency configured for the destination
Electrical Control
  • Electrical component brand can be specified
  • PLC optional
  • HMI / touchscreen optional
  • VFD optional
07 · SAFETY & ACCESS

Explosion Protection, Safety & Maintenance

  • Explosion vent panel
  • Flameless explosion venting device
  • Explosion-proof motor
  • Explosion-proof electrical cabinet
  • Spark arrestor / spark trap
  • Maintenance platform available as required
INTEGRATED TWO-STAGE FILTRATION

Integrated Cartridge + HEPA Dust Collector Module

7US can integrate primary cartridge filtration and secondary HEPA filtration into one modular collector body. The cartridge section and HEPA section are arranged vertically within the same structural module, creating a compact two-stage filtration unit rather than two separate machines connected by ductwork.

Cartridge + HEPA in One Cabinet
Vertically Integrated Two-Stage Filtration
No Separate HEPA Unit Required
One integrated module, engineered as one filtration system. The integrated arrangement reduces external duct connections and installation space. HEPA filter area, final pressure drop and fan selection are engineered together with the primary cartridge stage to maintain the required system airflow and final filtration performance.
Explosion-protection items are configurable components for project requirements. Final compliance scope and component certification should be confirmed for the destination market and application.
09 Applications & Delivery
Contents ↑
APPLICATION RANGE & PROJECT DELIVERY

Typical Applications & Product Views

Industrial cartridge dust collectors can be configured for a wide range of dry-dust and fume applications. Application suitability is determined by the actual dust characteristics, loading, filtration media, airflow and safety requirements — not by equipment appearance alone.

TYPICAL APPLICATIONS

Common Industrial Dust & Fume Duties

EHCDT and EHCDP modular collectors can be engineered for different process conditions after the dust source and operating requirements are confirmed.

Shot & Sand Blasting Grinding & Polishing Welding Fume Laser Cutting Metalworking Powder Handling Woodworking Foundry & Dry Process Dust
PROJECT DELIVERY

From Factory Preparation to Site Assembly

Large collectors are prepared as modular equipment for inspection, transport and practical field assembly. Site installation is normally completed by the customer or local contractor with drawings and technical guidance from 7US.

01 Factory Trial Assembly Fit and interfaces checked before shipment.
02 Modular Packing Sections prepared for practical transport.
03 Shipment Module dimensions coordinated with logistics.
04 Assembly Guidance Drawings and remote technical support available.

Additional Product Views

These examples show how the same modular collector platform can be adapted through structural reinforcement, material selection, fan integration, inlet protection and hopper configuration to suit different project requirements.
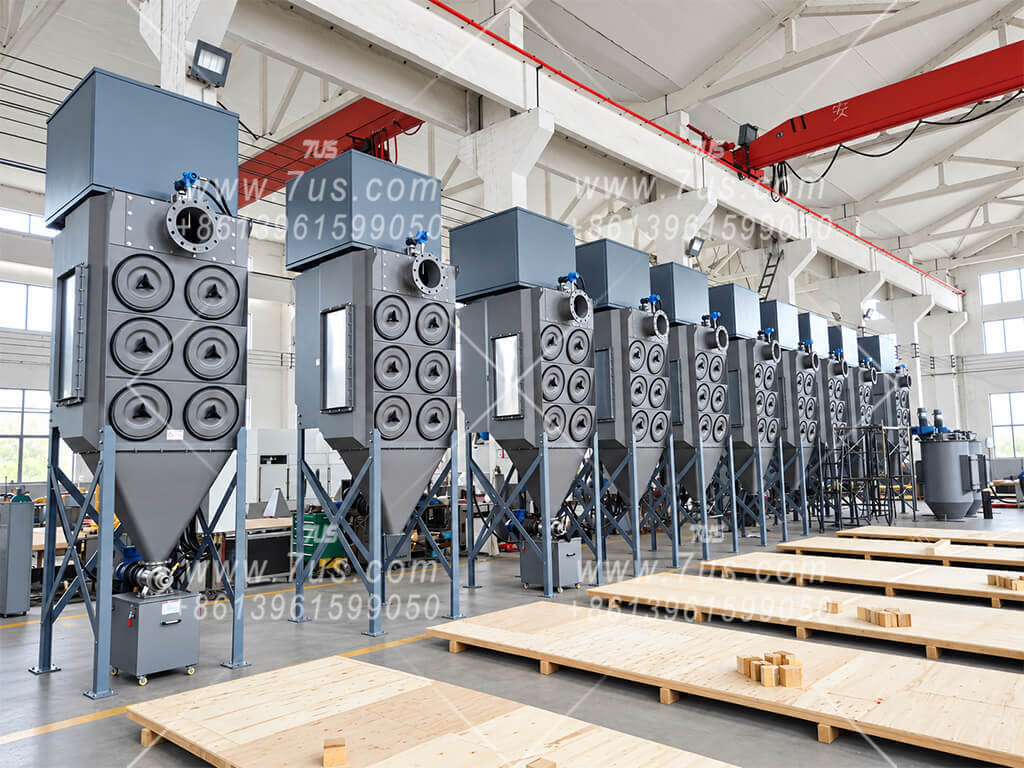
EHCDT2-4 high-negative-pressure cartridge dust collector
EHCDT2-4 High-Negative-Pressure Unit Single-unit collector with additional structural stiffeners for high-negative-pressure service.
EHCDT3-6 SS304 cartridge dust collector with explosion-protection configuration
EHCDT3-6 · SS304 Explosion-Protection Configuration SS304 construction with an explosion vent panel and the fan integrated into a top-mounted acoustic enclosure.
EHCDT4-64 modular cartridge dust collector
EHCDT4-64 Modular Unit Large modular collector with a wear-resistant inlet and two-stage hopper arrangement.
More application references and project photographs are available on request.
10 FAQ & Inquiry
Contents ↑
FINAL SELECTION QUESTIONS

Questions Buyers Usually Ask

Most project details can be finalized after the required airflow, dust conditions, installation space and system scope are confirmed. The questions below cover the items most commonly discussed before quotation and drawing approval.

How do I choose between EHCDT and EHCDP?

Both series use the same modular filtration and pulse-cleaning concept. EHCDT uses inclined cartridges to support more effective dust shedding, while EHCDP uses horizontal side-insertion cartridges and is available in 2-, 3-, 4- and 5-level configurations. Final selection depends on the dust, available height / width, maintenance access and preferred module arrangement.

Can the collector be supplied without a fan?

Yes. The collector body can be supplied separately, or 7US can configure the fan and control package after the required airflow, system pressure, voltage and frequency are confirmed.

Can material, coating color and structural specifications be customized?

Yes. Q235 carbon steel, SS304 and SS316L are available. Coating color can be specified by the customer, and plate thickness, reinforcement and structural strengthening can be customized for special service conditions.

Can you provide GA and DWG drawings?

Typical drawings can be used during product selection. Detailed GA / DWG project drawings can be prepared after the final configuration, interfaces and order requirements are confirmed.

Can HEPA filtration be integrated into the same collector body?

Yes. 7US can integrate primary cartridge filtration and secondary HEPA filtration vertically within the same modular collector body, instead of using a separate HEPA machine connected by ductwork. HEPA area, pressure drop and fan selection are engineered together with the primary cartridge stage.

What explosion-protection options are available?

Available options include explosion vent panels, flameless explosion venting devices, explosion-proof motors, explosion-proof electrical cabinets and spark-arresting components. Final compliance scope and component certification should be confirmed for the actual application and destination market.

Preparing the public shell…